QintelliM heavy-duty deburring, heavy-slag removal, and edge finishing equipment helps machinery manufacturers process thick plates, structural parts, welded components, and laser- or plasma-cut metal parts with more consistent results.
Case Details
Heavy Machinery Deburring, Heavy-Slag Removal and Edge Finishing Solutions
Heavy machinery manufacturers process thick plates, structural brackets, welded components, frames and thermal-cut parts that can carry large slag, heavy burrs, sharp edges and oxide residue. These defects increase manual grinding time and can affect handling, welding preparation, coating preparation and downstream assembly.
QintelliM, a metal deburring and surface finishing equipment manufacturer, configures heavy-duty systems for alloy-hammer slag removal, sanding-belt deburring, rotary roller brush edge rounding and surface preparation. The process must be selected from the actual cutting method, plate thickness, slag size, part weight, surface condition and required production rate.
Heavy Machinery Parts and Typical Finishing Problems
Part or process
Typical defect
Finishing priority
Plasma-cut and flame-cut thick plates
Large attached slag, rough cut edges and heavy burrs
Remove heavy slag before finer sanding-belt deburring
Structural brackets and gussets
Sharp external edges, hole burrs and inconsistent cut quality
Deburr and create the specified edge rounding before handling or coating
Welded machinery components
Oxide, scale, spatter or uneven surfaces around the finishing area
Prepare the required surface without replacing application-specific weld cleaning
Wide machine panels and base plates
Long processing width and high material-removal demand
Select stable multi-belt deburring and a suitable working width
When to Use C Heavy-Slag Removal
A C heavy-slag removal station uses alloy-hammer tooling to detach large slag from plasma-cut, flame-cut or other suitable thermal-cut ferrous parts. This stage should be considered before R sanding-belt deburring when the slag is too large or too strongly attached for a standard deburring pass.
The C station is not a substitute for every grinding operation. Workpieces with only normal laser-cut burrs may be better matched to R or R-R deburring. Sample testing determines whether the correct route is C, C-R, C-R-S-R or a belt-based configuration without C.
Heavy-Duty Process Routes
Process route
Station function
Typical use
C-R
Alloy-hammer heavy-slag removal followed by sanding-belt deburring
Plasma-cut or flame-cut parts with large slag and remaining burrs
C-R-S-R
Heavy-slag removal, first deburring, rotary roller brush edge rounding and final R processing
Thick parts that also require more consistent rounded edges
R-R
Two sanding-belt deburring stages
Heavy burr removal or surface preparation without large attached slag
R-R-R
Three deburring stages configured for higher material-removal demand
Wide or high-volume parts requiring multiple belt stages after testing
Conveyor Holding for Heavy Parts
An M magnetic adsorption platform is commonly considered for suitable ferrous plates because it supports stable conveying during heavy-duty processing. A vacuum adsorption platform may be used for suitable non-magnetic workpieces when the available surface area and part flatness provide enough holding force. An A-M platform combines magnetic and vacuum holding. Its actual layout and effective holding areas are project-specific and should be confirmed for the workpiece and application.
Part weight, smallest dimensions, holes, cutouts, distortion and conveyor contact area must be checked. Very heavy, uneven or unstable parts may require a specific loading method and application review before machine selection.
Heavy slag, sanding debris and fine dust do not create the same collection requirement. The dust-collection method must be selected from the workpiece material, particle condition, number of connected machines, airflow requirement and local safety rules. Sanding belt specification, alloy-hammer tooling and maintenance intervals should be confirmed from the actual application rather than estimated only from plate thickness.
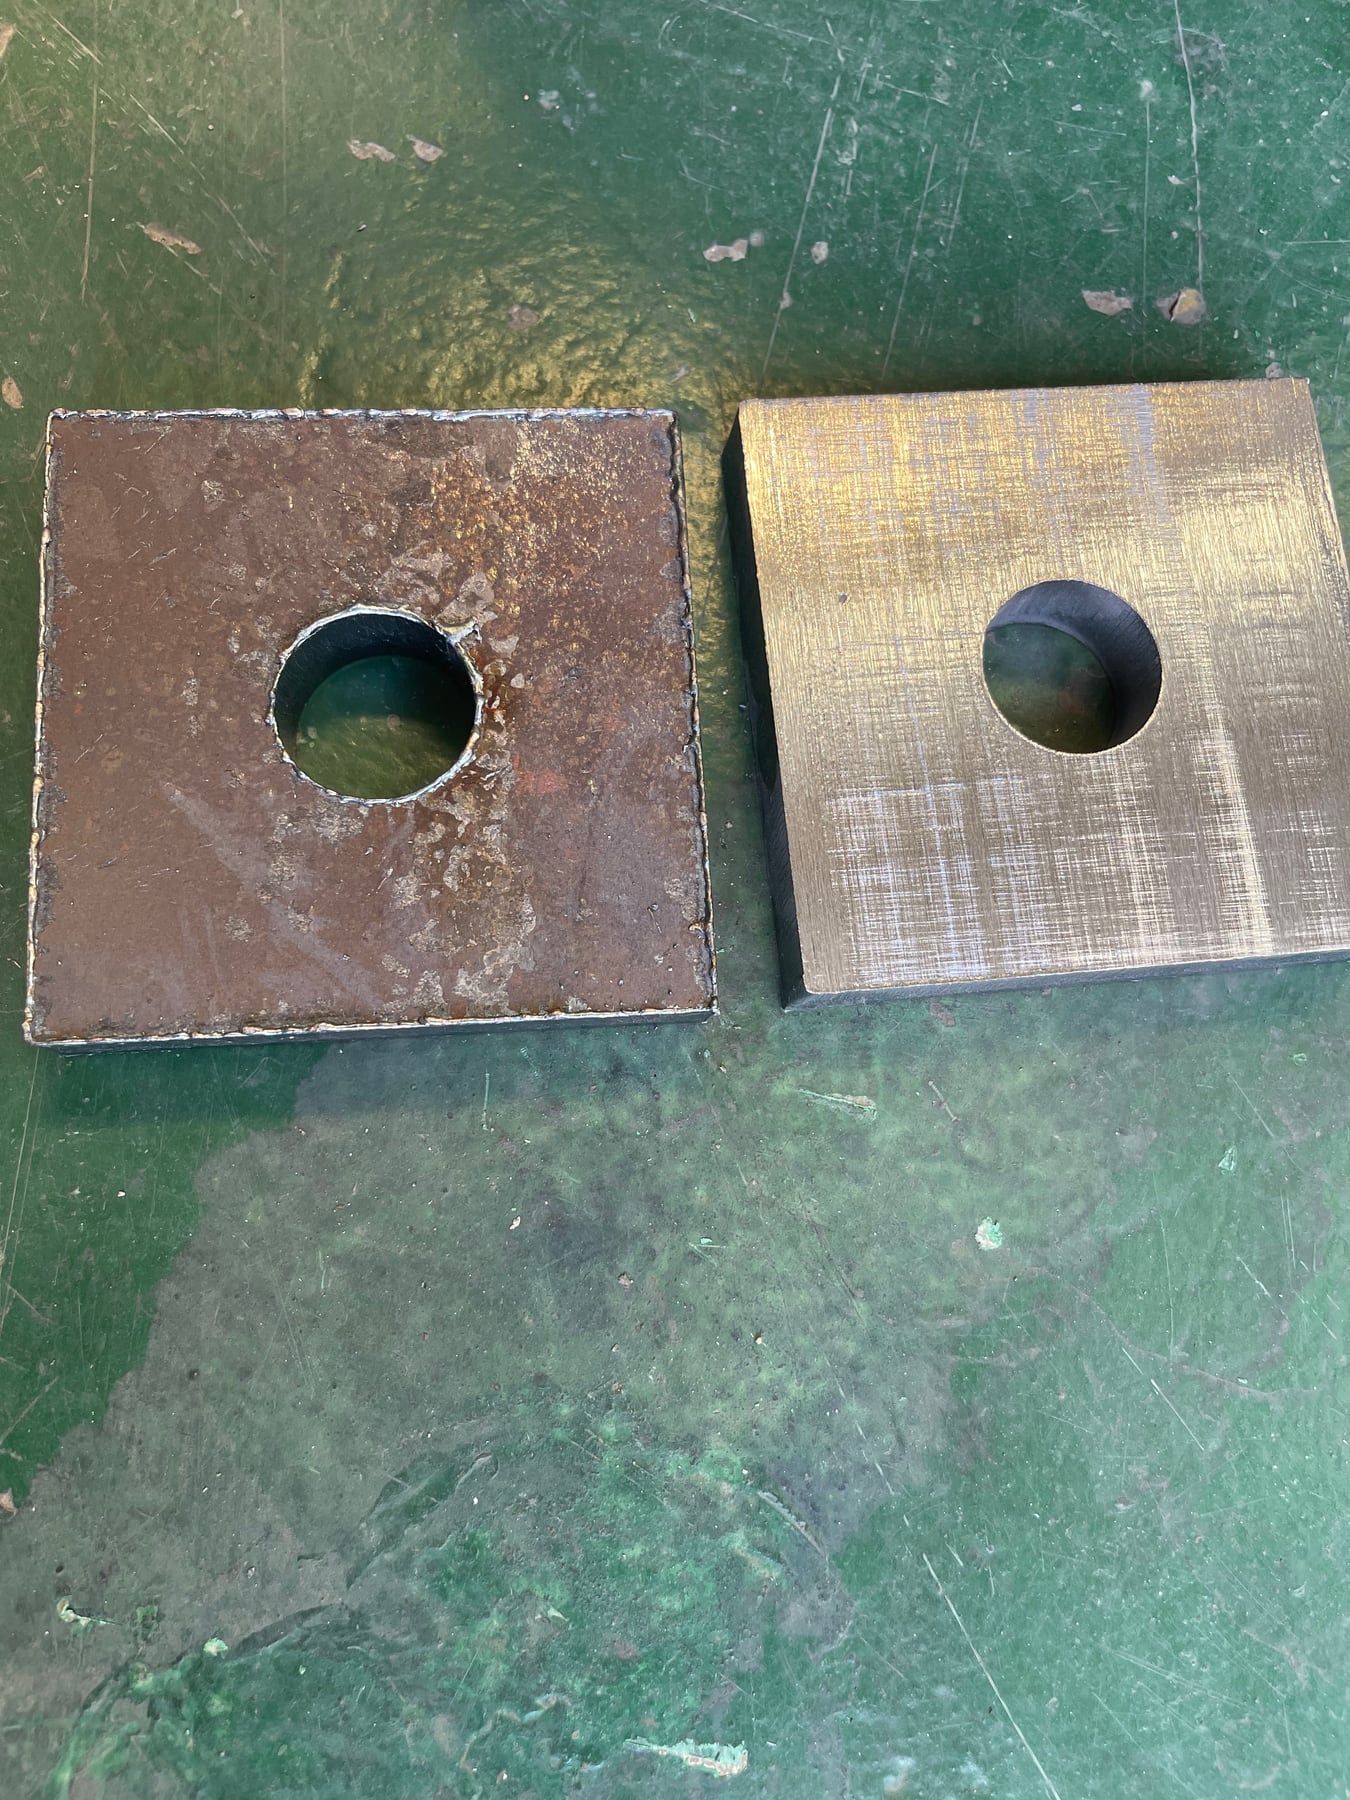
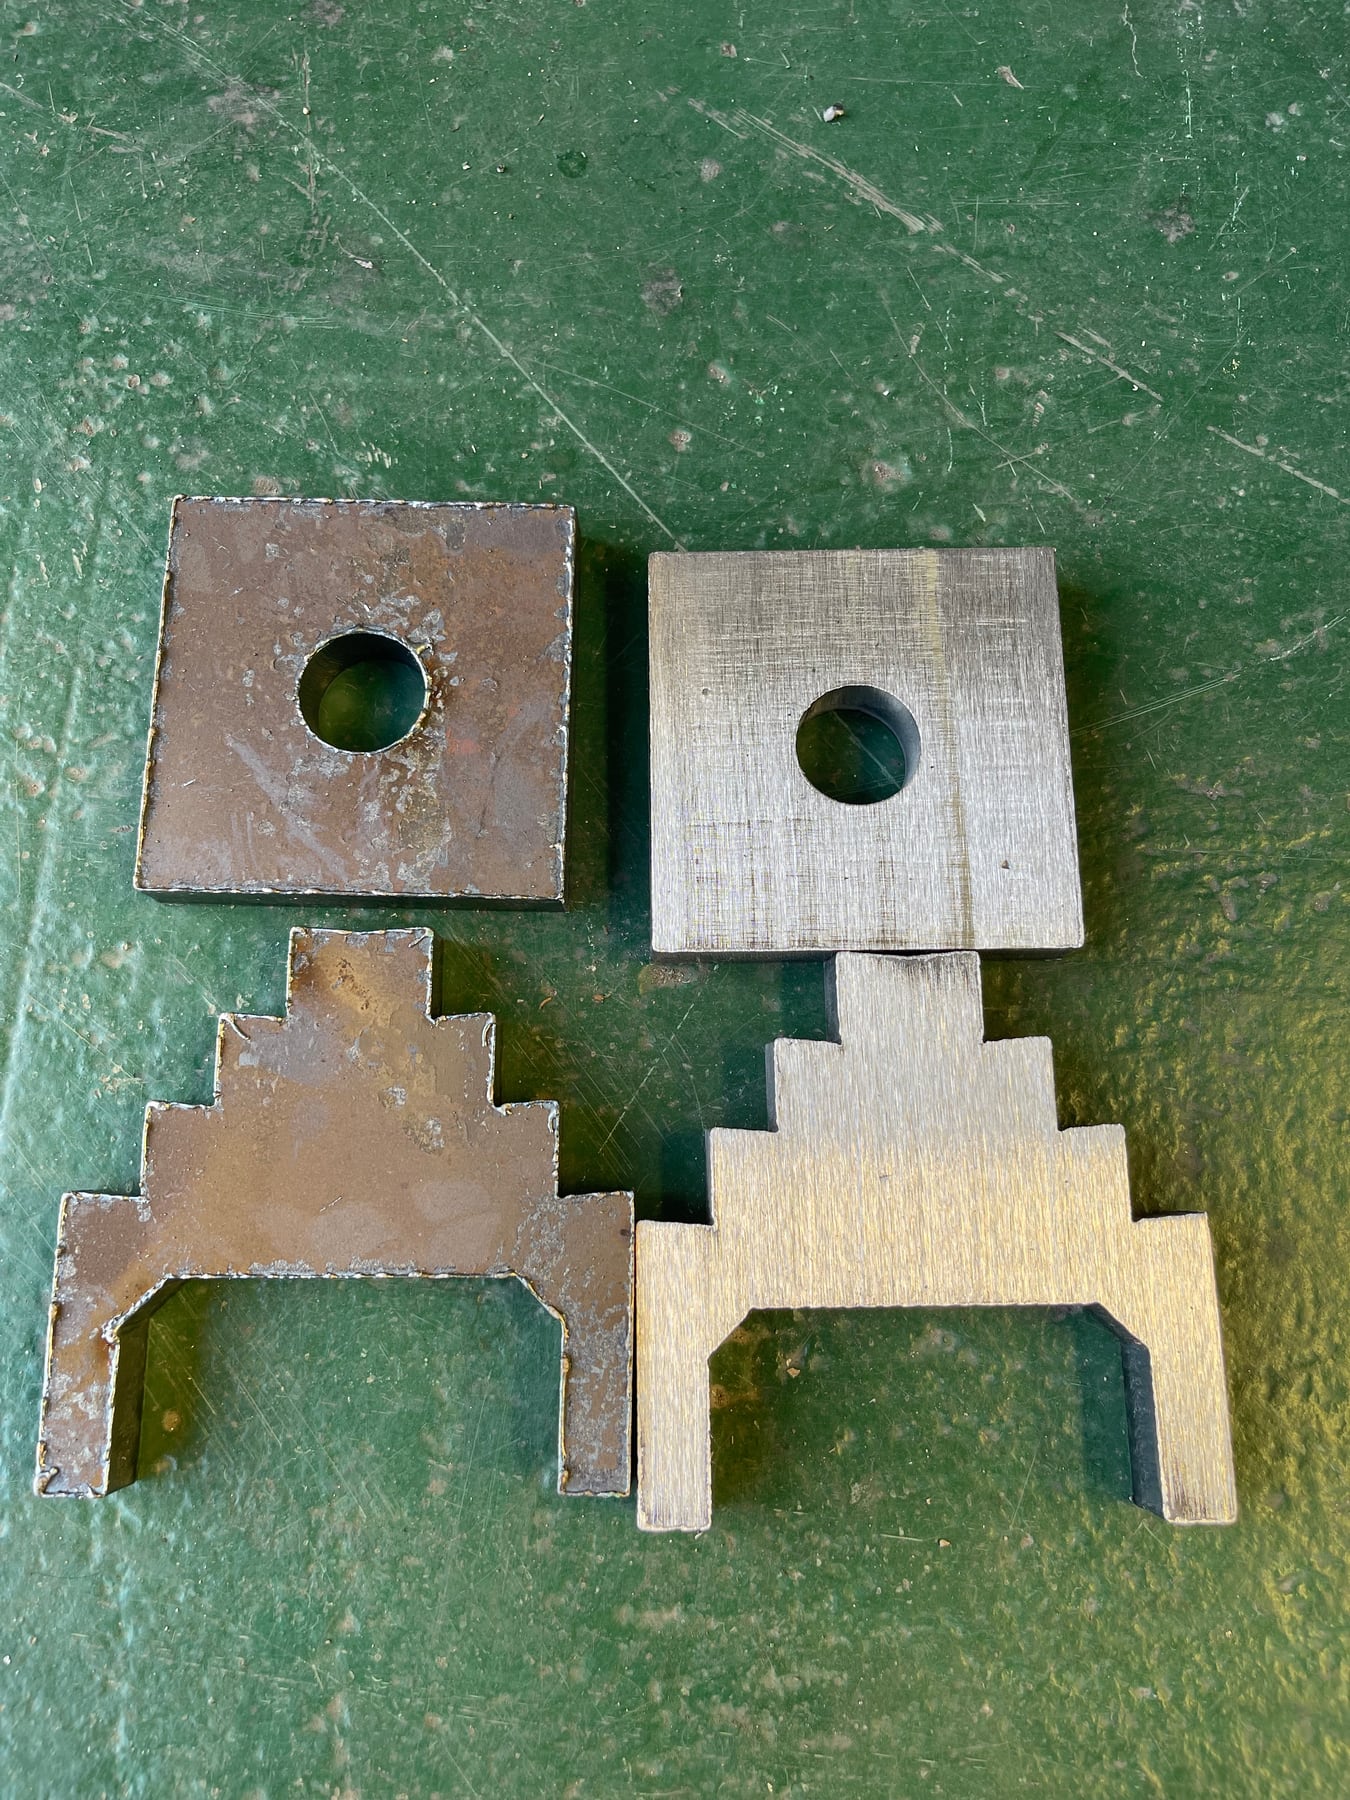
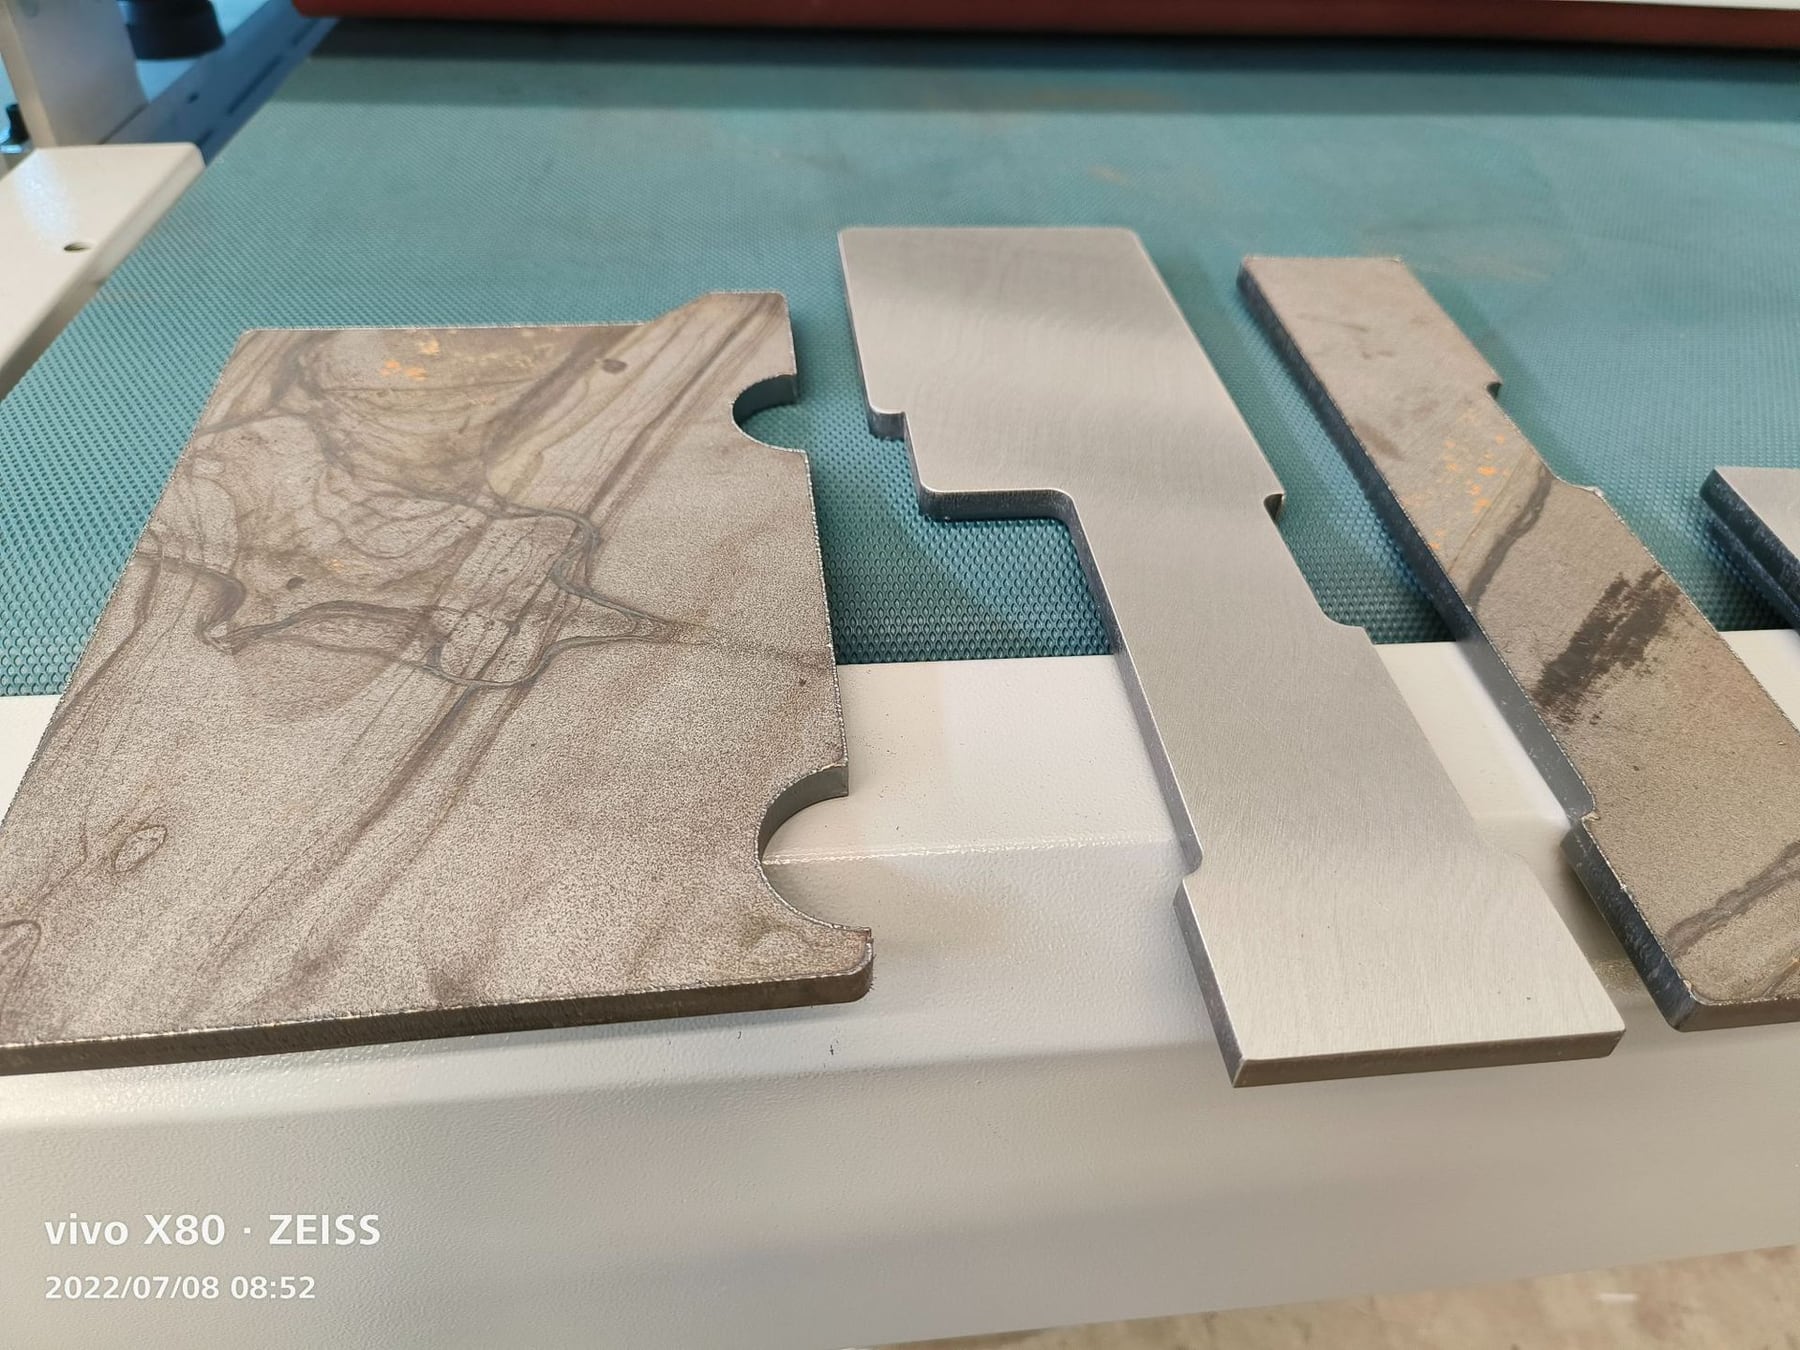
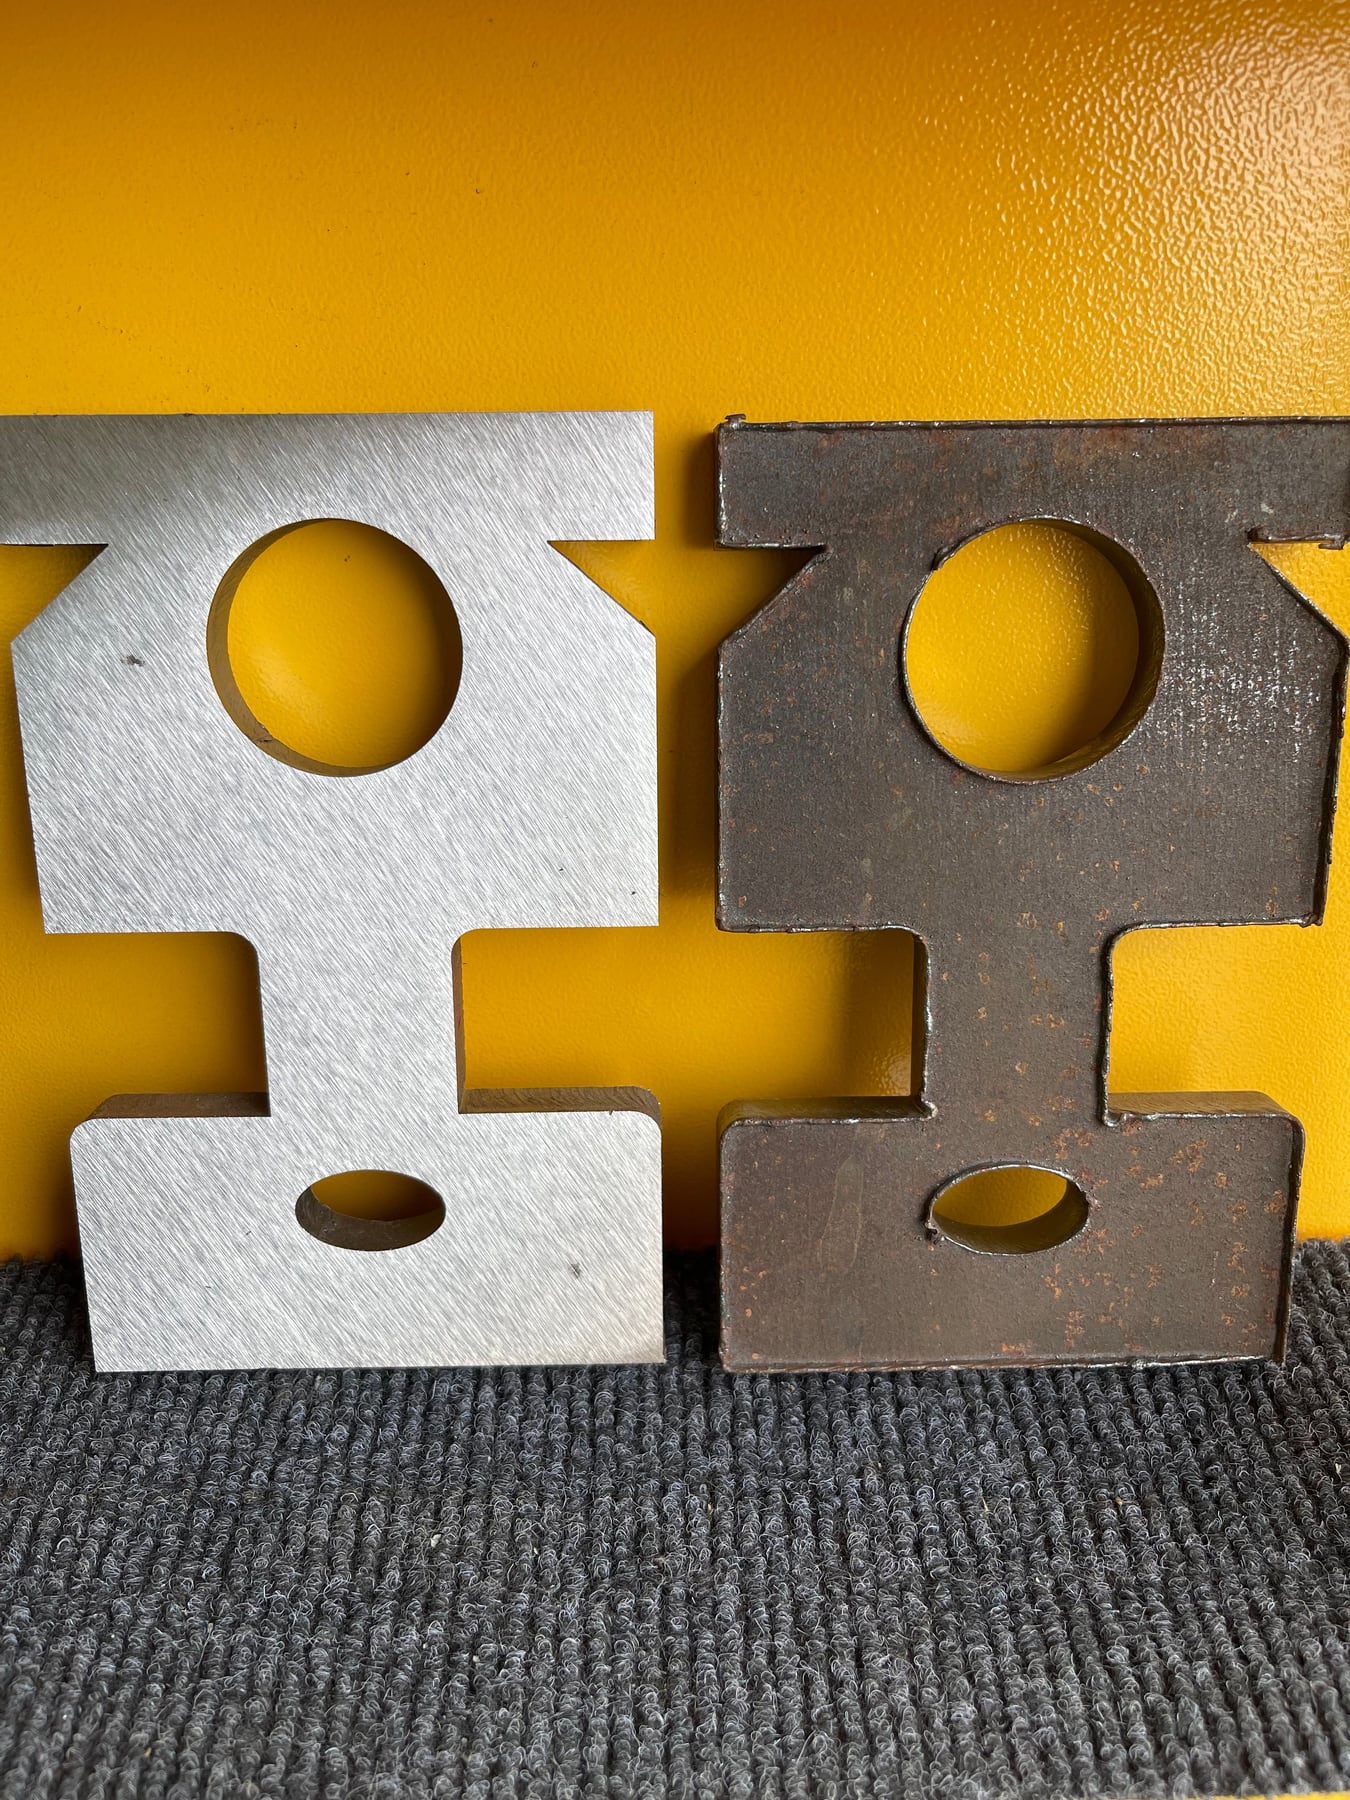
Photographs from QintelliM customer sample trials. Results depend on the material, incoming condition and finishing requirements.
Square and stepped plate samples
Comparison views document the original and finished surfaces, holes and contours of square and stepped plate samples.
Original sample, left · Finished sample, rightOriginal samples, left · Finished samples, right
Surface finishing on complex profiles
Separate profiled samples illustrate original and finished surface conditions.
Original sample, left · Finished sample, centreFinished sample, left · Original surface, right
These photographs illustrate sample appearance. Material grade, dimensions, edge radius and surface requirements should be confirmed through sample evaluation and inspection.
Can a normal sanding-belt deburring machine remove heavy plasma-cut slag?
Not always. Large attached slag should be evaluated for a C alloy-hammer heavy-slag removal stage before R sanding-belt deburring. Sample testing is required because slag size and attachment vary with cutting parameters and material.
Does every thick plate need a C station?
No. Plate thickness alone does not determine the station. A thick laser-cut part with normal burrs may use R or R-R processing, while a thinner plasma-cut part with strongly attached slag may need C-R.
Can the same machine also create edge rounding?
Yes, when an S edge-rounding station with rotary roller brush tooling is included in a suitable sequence such as C-R-S-R. The achievable result depends on part geometry, material, burr condition and the specified edge-radius target.
Information Needed for a Heavy Machinery Process Recommendation
Material grade, plate thickness and part weight.
Plasma, flame, laser or other cutting method.
Photos of slag attachment, burr height and both sides of the part.
Minimum and maximum workpiece dimensions.
Required edge result, surface condition and downstream process.
Daily volume, loading method, working width and dust-collection requirements.
Recommended Finishing Workflow for This Application
Use the information below to match the case application with a practical QintelliM deburring, edge rounding, grinding, brushing, slag removal, oxide removal or dust collection configuration.
Burrs after laser cutting, sharp outer edges, small inner holes, oxide layers before coating, inconsistent manual grinding and dust safety risks.
BurrsSharp EdgesOxide Layer
Recommended Processes
Combine abrasive belt grinding, edge rounding brushes, brushing or polishing rollers, heavy-slag removal and dust collection according to the real workpiece condition.
DeburringEdge RoundingSurface Finishing
Selection Information Needed
Share material, cutting method, thickness, workpiece size, burr condition, required finish, capacity target, dust characteristics and local project requirements for wet dust collection review.
MaterialSizeCapacity
QintelliM Station Logic
Configurations can be adjusted with process stations and conveyor platforms to fit different industries and workpiece requirements. Working widths can be customized at 450 / 630 / 800 / 1000 / 1300 / 1600 mm.
RAbrasive belt grinding for burr and oxide removal.
SBrush edge rounding for outer edges and inner holes.
CAlloy hammer station for heavy slag removal.
WBrushing or polishing roller for surface finishing.
AVacuum conveyor platform for non-magnetic parts.
MMagnetic conveyor platform for carbon steel parts.
A-MHybrid platform for mixed material production.
DustWet dust collection configuration for the actual machine and application.
QintelliM currently supplies wet dust collection systems only. For QintelliM deburring, grinding, edge-rounding and surface-finishing machine projects, wet dust collection is our current standard recommended solution. Final dust-control configuration depends on the actual material, dust characteristics, machine process, system design, installation conditions and applicable local requirements.