QintelliM precision deburring, edge rounding, brushing, and polishing solutions help aerospace component manufacturers improve burr control, surface consistency, and finishing repeatability for demanding metal parts.
Case Details
Aerospace Metal Deburring and Precision Surface Finishing
Aerospace metal parts often require controlled burr removal, repeatable edge finishing and stable surface quality before assembly, coating or inspection. The correct process depends on the material, part thickness, geometry, cutting or machining method, edge-radius target and the condition of visible surfaces.
QintelliM, a metal deburring and surface finishing equipment manufacturer, configures automated processes for aerospace-related brackets, panels, enclosures, frames, fixtures and other precision metal components. The objective is to reduce manual finishing variation while protecting the workpiece and keeping the process suitable for later inspection and customer-specific quality controls.
Where Burrs and Edge Problems Occur
Laser cutting, punching, stamping, drilling and machining can leave different types of burrs. Thin panels may have sharp cut edges or local distortion risk. Machined components may have fine burrs around holes, slots and contours. Visible panels can also require a consistent directional finish after the primary deburring step.
Typical aerospace-related part
Common finishing issue
Process objective
Thin aluminum panels and covers
Sharp edges, fine burrs and unstable holding
Controlled deburring with suitable vacuum adsorption and limited processing pressure
Stainless steel brackets and frames
Cutting burrs, oxide residue and inconsistent edges
Remove burrs, create controlled edge rounding and prepare the part for the next operation
Machined housings, plates and fixtures
Fine burrs around holes, slots and machined contours
Reduce residual burrs without unnecessary material removal from critical surfaces
Visible panels and interior metal components
Uneven brush marks, scratches or inconsistent appearance
Add a controlled W brushing or polishing process when the required finish has been confirmed
Recommended QintelliM Station Logic
An R deburring station uses sanding belt consumables for initial burr removal and surface preparation. An S edge-rounding station uses rotary roller brush tooling to create more consistent rounded edges around external contours and accessible internal features. A W station can use a brushing roller or polishing roller when a controlled visible finish is required.
R: sanding-belt deburring for cutting burrs, fine surface defects and preparation before later finishing.
S: rotary roller brush edge rounding for safer and more consistent edges; this is edge rounding, not chamfering.
W: brushing or polishing for the required directional or refined surface appearance.
R-S or R-R-S: useful when initial burr removal must be completed before controlled edge rounding.
R-S-W: considered when the part needs deburring, edge rounding and a final brushing or polishing step in one line.
Choosing the Conveyor Platform
Workpiece holding is especially important for thin, light or mixed aerospace-related parts. The conveyor platform must be selected according to material, dimensions, flatness and the available contact area.
A vacuum adsorption: suitable for many aluminum, non-magnetic or thin parts when the workpiece provides enough surface area for stable holding.
M magnetic adsorption: suitable for compatible ferrous workpieces that can be held securely by a magnetic conveyor.
A-M combined platform: combined magnetic and vacuum holding, with project-specific layouts and effective holding areas confirmed for the actual workpieces and applications.
Representative sample testing is necessary before selecting a machine configuration. QintelliM should review the actual workpiece material, thickness range, maximum and minimum dimensions, cutting or machining process, burr condition, required edge result, visible-surface requirement and expected throughput. Thin parts, formed parts and components with limited conveyor contact may require additional holding tests.
The test result should be checked against the buyer's drawing, inspection method and downstream process. Machine finishing can support a repeatable manufacturing workflow, but the final acceptance standard remains the responsibility of the manufacturer and its customer. Read why sample testing matters before configuring a metal deburring machine.
REAL SAMPLE FINISHING
Customer Sample Finishing Results
Photographs from QintelliM customer sample trials. Results depend on the material, incoming condition and finishing requirements.
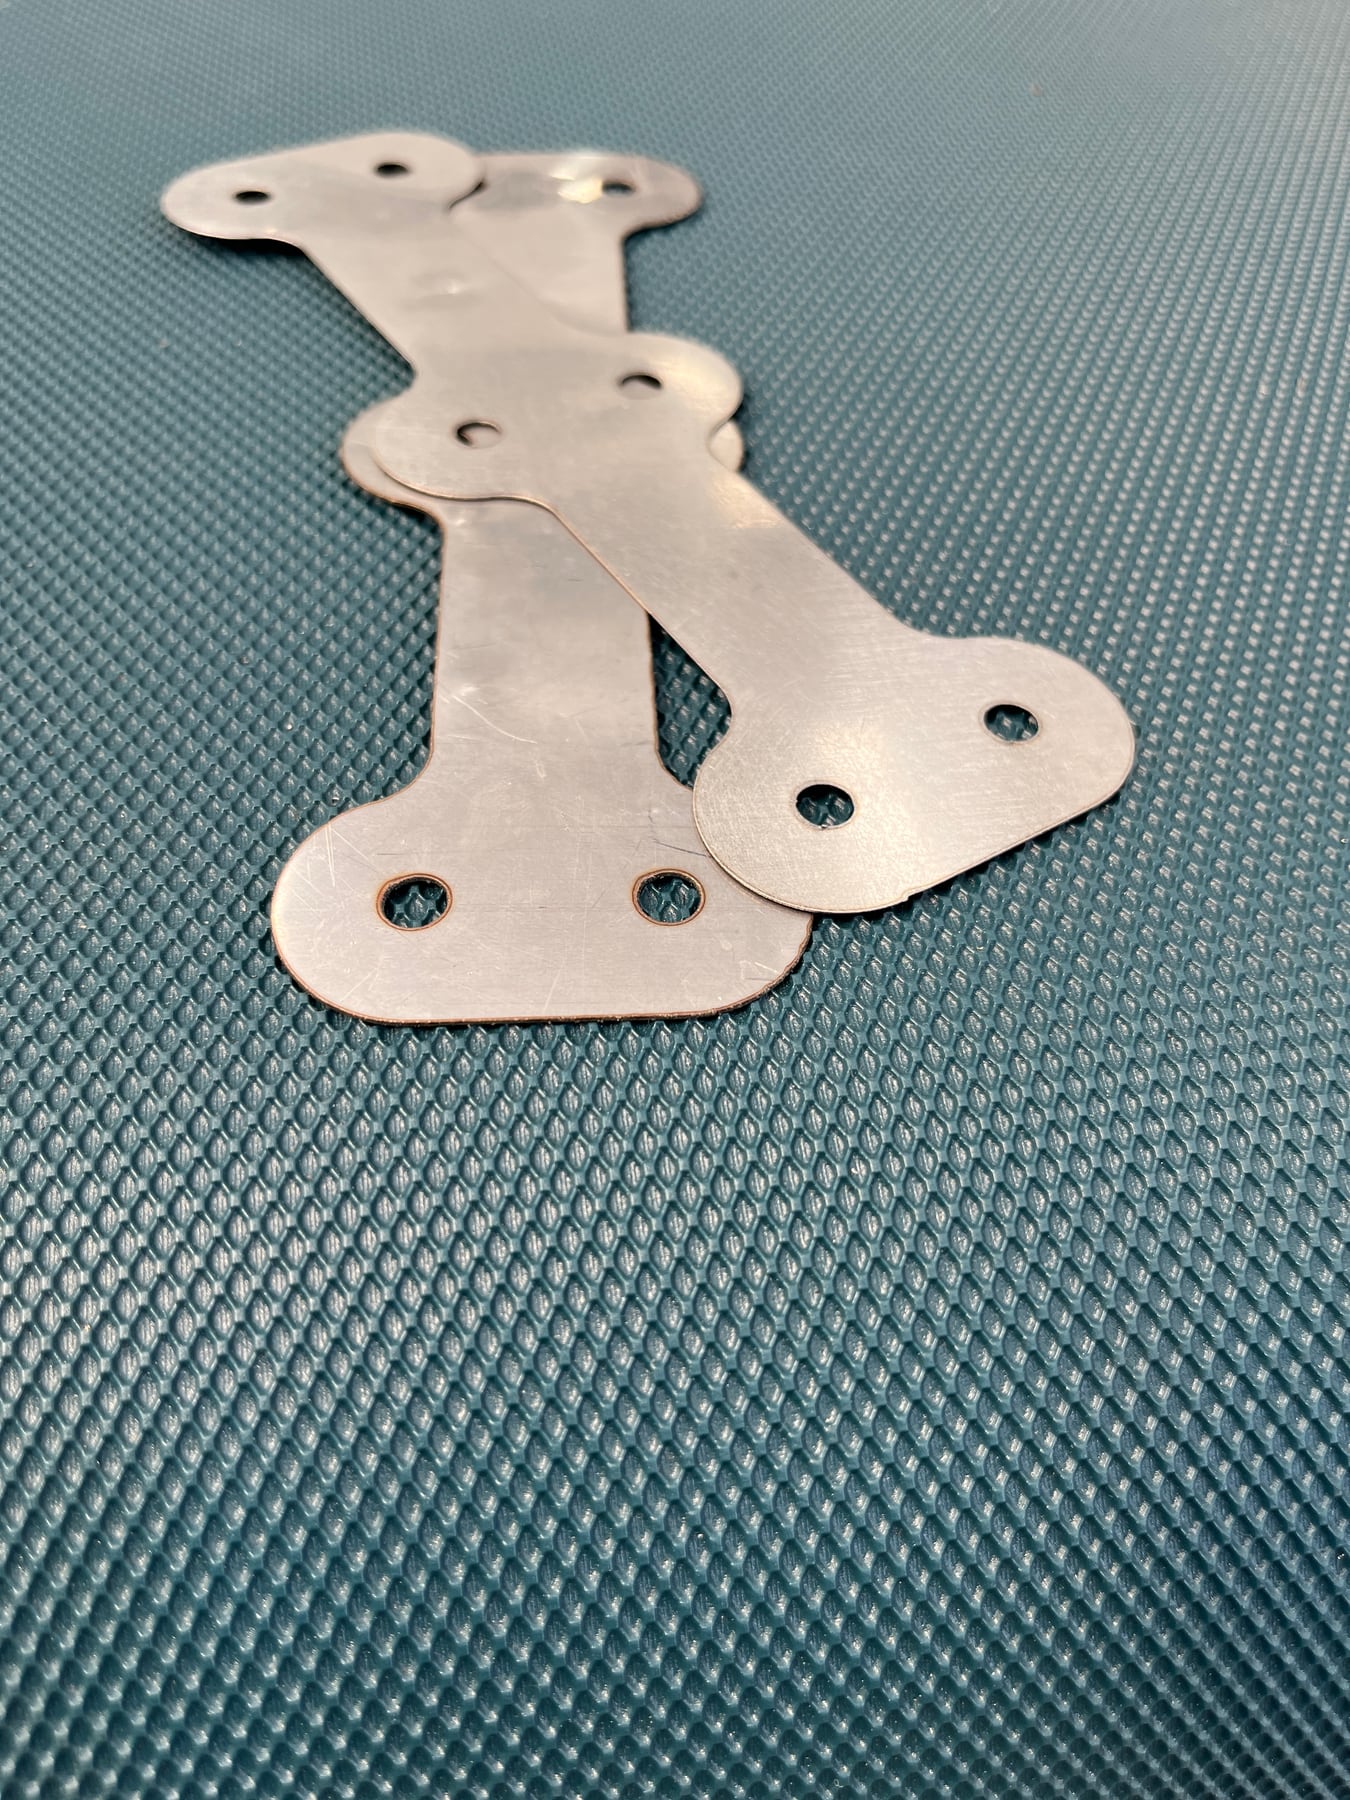
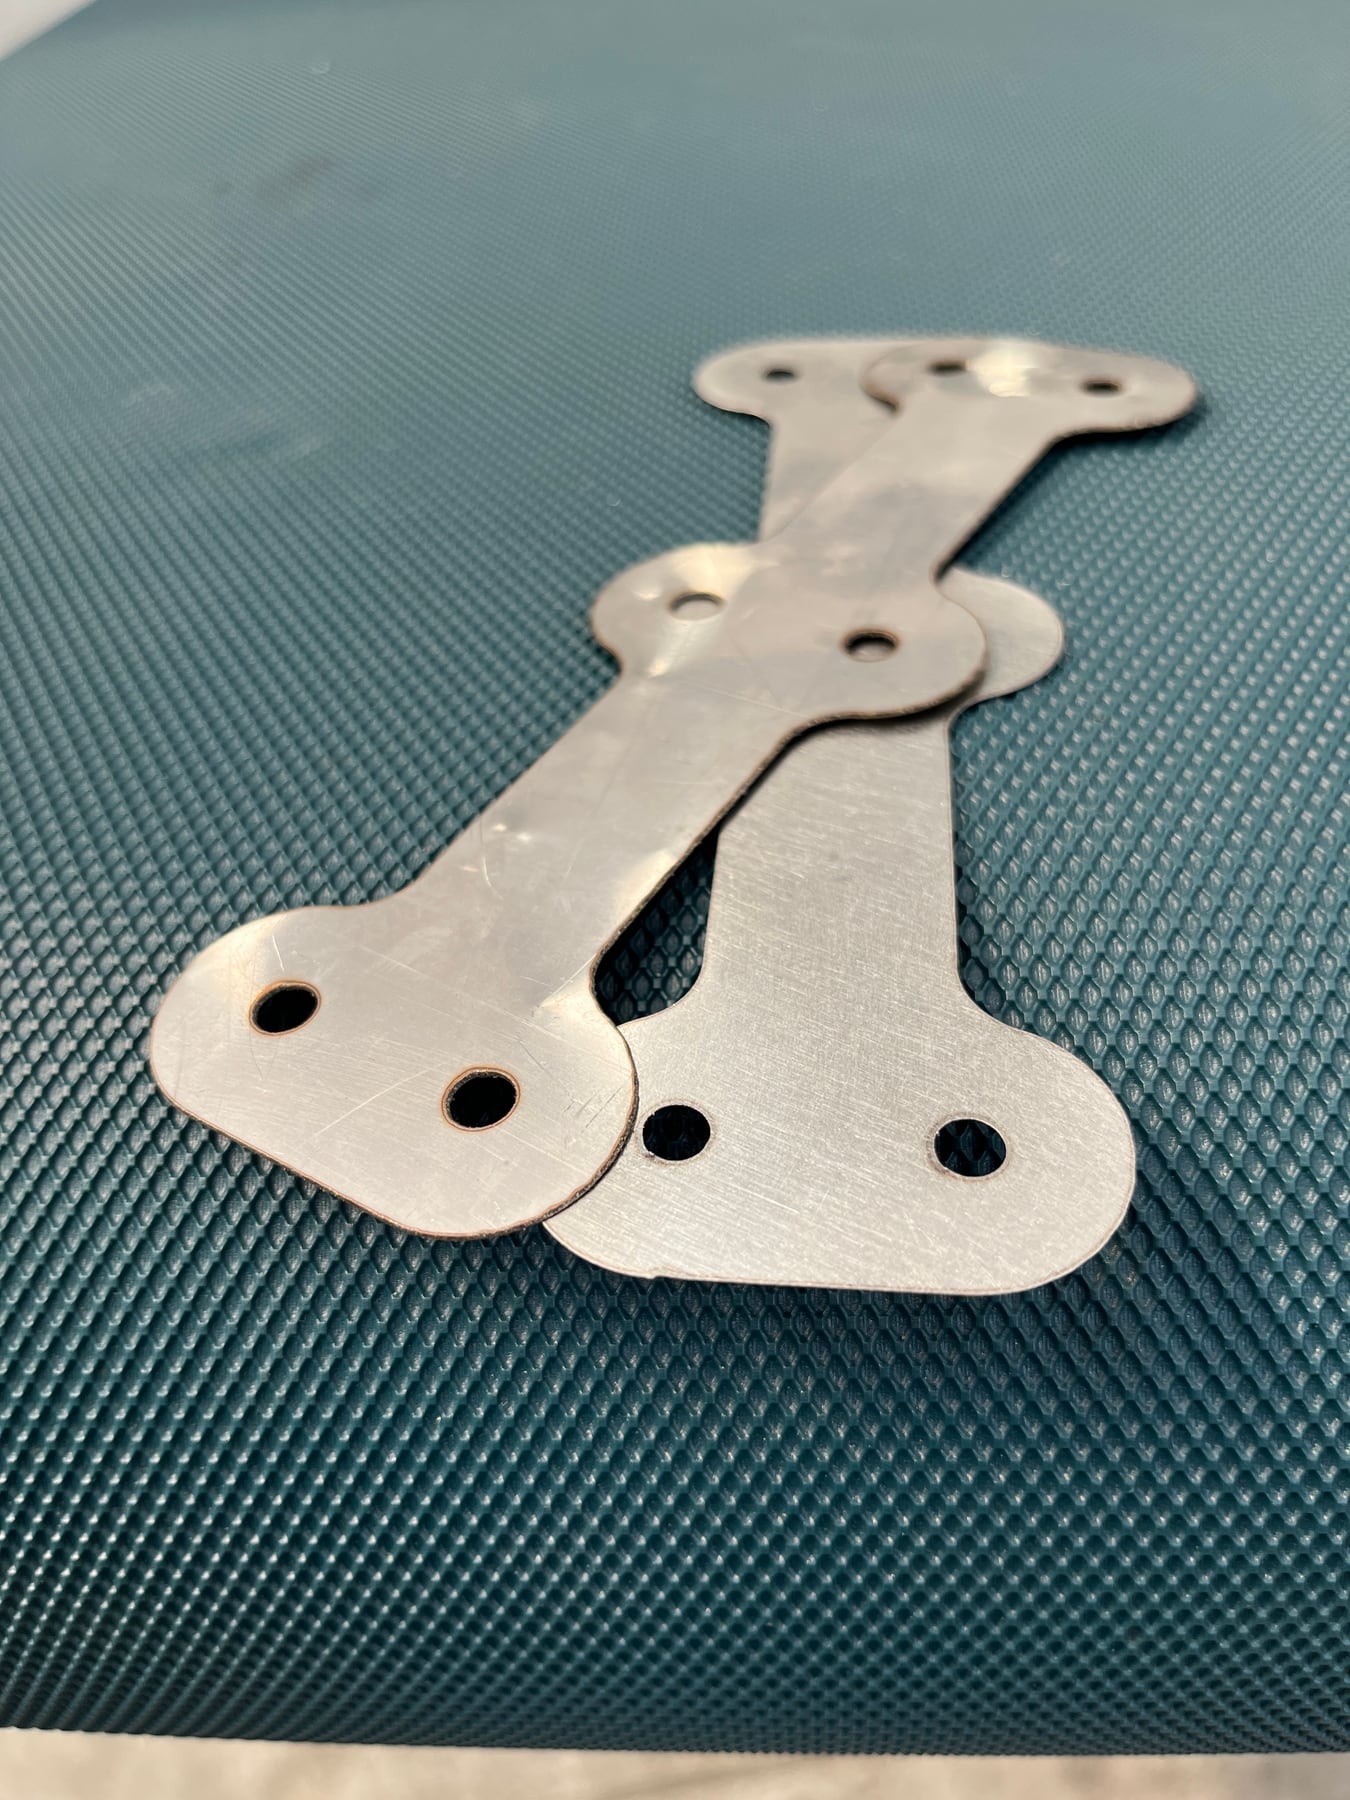
Slender profiled plate samples
Two views document the original and finished surfaces of slender profiled plate samples.
Slender profiled sample comparisonAdditional view of the profiled sample set
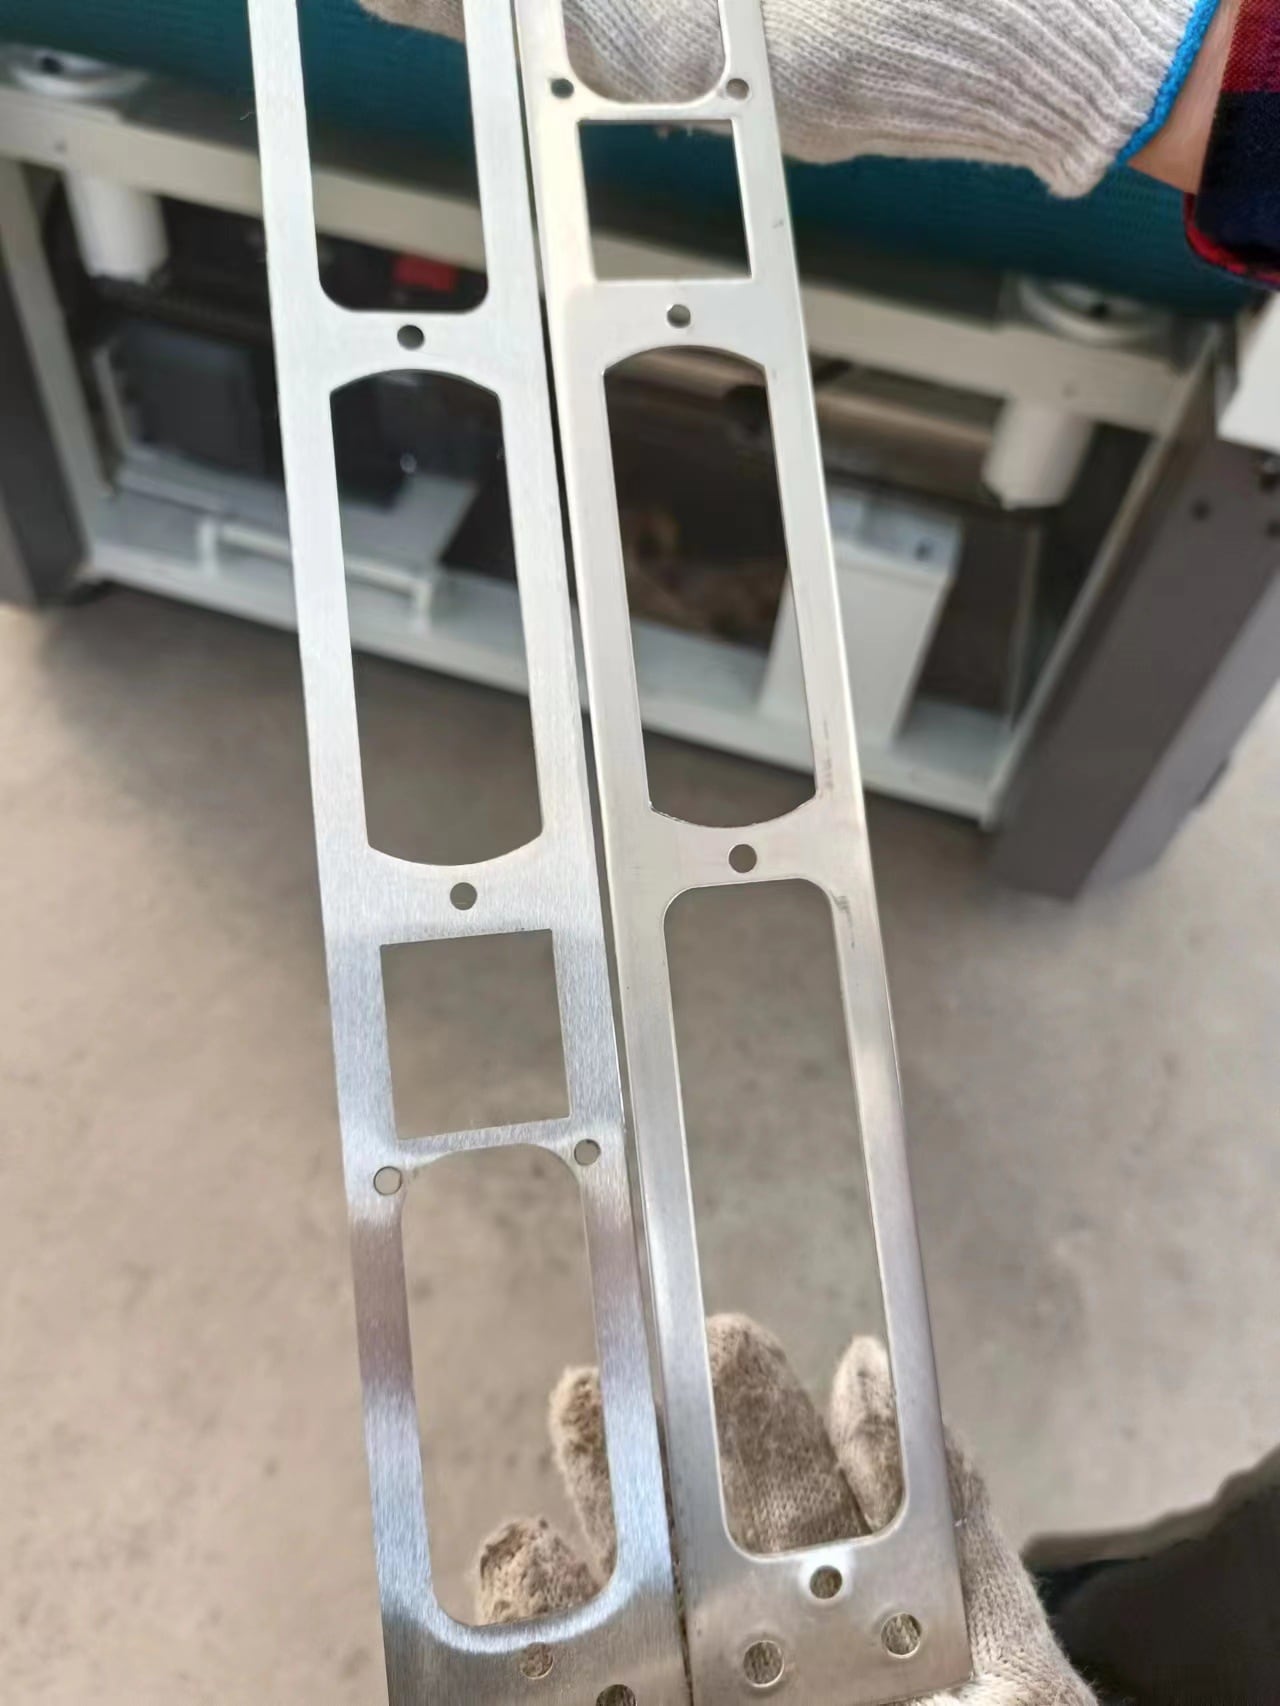
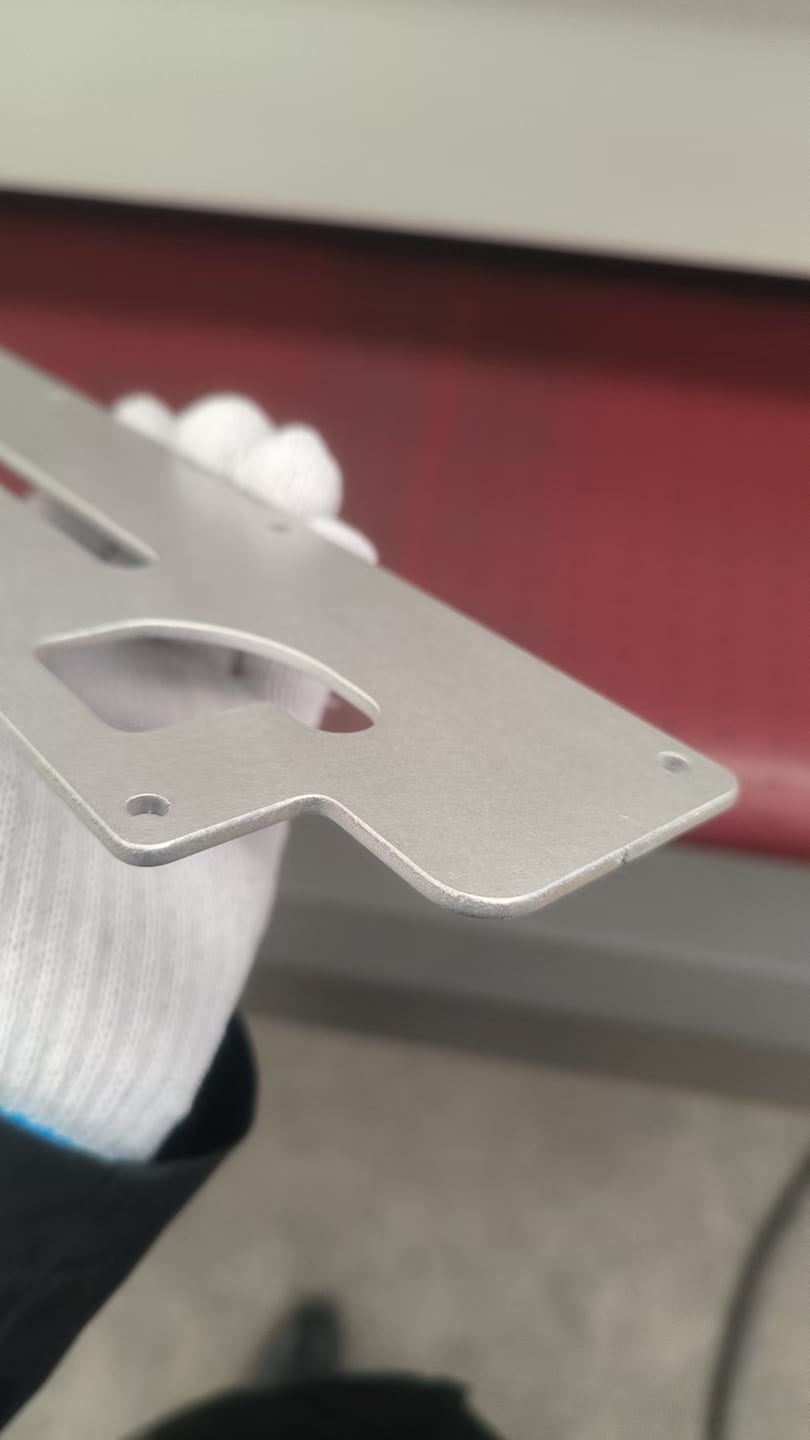
Frame and thin-plate edge details
Separate sample photographs show long frame openings and a thin-plate edge in close-up.
Frame samples — surfaces and openingsThin-plate contour and edge detail
These photographs illustrate sample appearance. Material grade, dimensions, edge radius and surface requirements should be confirmed through sample evaluation and inspection.
Can thin aluminum aerospace-related panels be processed automatically?
They may be suitable when the vacuum adsorption area, part flatness, feed stability and processing pressure have been validated with representative samples. Very small, formed or flexible parts require additional testing before a machine recommendation is confirmed.
Should every aerospace metal part use the same station sequence?
No. A fine machining burr may need a different process from a laser-cut bracket or a visible panel. The station sequence should be selected from the actual burr height, edge requirement, material and surface target.
Does automated deburring certify an aerospace component?
No. QintelliM equipment performs deburring and surface finishing operations. It does not by itself certify airworthiness, aerospace compliance, material conformity or final part acceptance. These requirements must be defined and verified by the manufacturer and relevant customer or authority.
Information Needed for an Aerospace Deburring Recommendation
Workpiece material and material condition.
Minimum and maximum part dimensions and thickness.
Cutting, punching, stamping, drilling or machining process.
Photos of the burr, edge and visible surface.
Required edge result, surface finish and inspection method.
Expected throughput, working width and automation requirement.
Recommended Finishing Workflow for This Application
Use the information below to match the case application with a practical QintelliM deburring, edge rounding, grinding, brushing, slag removal, oxide removal or dust collection configuration.
Burrs after laser cutting, sharp outer edges, small inner holes, oxide layers before coating, inconsistent manual grinding and dust safety risks.
BurrsSharp EdgesOxide Layer
Recommended Processes
Combine abrasive belt grinding, edge rounding brushes, brushing or polishing rollers, heavy-slag removal and dust collection according to the real workpiece condition.
DeburringEdge RoundingSurface Finishing
Selection Information Needed
Share material, cutting method, thickness, workpiece size, burr condition, required finish, capacity target, dust characteristics and local project requirements for wet dust collection review.
MaterialSizeCapacity
QintelliM Station Logic
Configurations can be adjusted with process stations and conveyor platforms to fit different industries and workpiece requirements. Working widths can be customized at 450 / 630 / 800 / 1000 / 1300 / 1600 mm.
RAbrasive belt grinding for burr and oxide removal.
SBrush edge rounding for outer edges and inner holes.
CAlloy hammer station for heavy slag removal.
WBrushing or polishing roller for surface finishing.
AVacuum conveyor platform for non-magnetic parts.
MMagnetic conveyor platform for carbon steel parts.
A-MHybrid platform for mixed material production.
DustWet dust collection configuration for the actual machine and application.
QintelliM currently supplies wet dust collection systems only. For QintelliM deburring, grinding, edge-rounding and surface-finishing machine projects, wet dust collection is our current standard recommended solution. Final dust-control configuration depends on the actual material, dust characteristics, machine process, system design, installation conditions and applicable local requirements.