How to Reduce Manual Grinding with a Deburring Machine and a Repeatable Process
Learn how to evaluate manual grinding tasks for machine processing, validate representative parts, define acceptance criteria and control process changes for repeatable production.
Mar 27th,202551 Views
Engineering Process Guide · Manual to Machine
Direct answer: Manual grinding should not be replaced simply because a machine is available. First document which part features are currently processed by hand, the incoming burr or surface condition, the required result and any areas that must remain protected. Then evaluate which operations can be transferred to R, S or W machine processes, confirm the result with representative parts, record the approved process and recheck the first piece after meaningful consumable or process changes. Some features may still require manual finishing if machine access, holding or the required result cannot be verified.
Originally published: March 27, 2025. Rebuilt as an engineering process guide: September 17, 2026.
The process: Manual baseline → Machine reachability → R / S / W process logic → Representative parts → Acceptance criteria → Approved process record → Consumable change → First-piece verification.
When Manual Grinding Becomes Difficult to Control
Consider a machine-processing review when repeat batches need consistent results but the current method is difficult to describe or reproduce. Differences between operators, results that depend heavily on individual experience and recurring uncertainty about whether a feature is acceptable are useful reasons to review the process.
These observations are reasons to investigate, not proof that automation is the best choice. Document the actual work and the required result before deciding which steps to transfer.
Start with a Manual Baseline
The table below is a recommended project record. It is a framework for an application review, not a statement that all QintelliM customers currently use this record.
Record
What to Capture
Part / batch
Representative part or part identity and the relevant batch.
Manual step
What is currently processed by hand.
Incoming condition
Burr, sharp edge, surface condition or another issue to be addressed.
Feature
External edge, hole, slot, surface or another specific location.
Required result
The agreed edge or surface acceptance requirement.
Protected area
Areas that must not be changed.
Current variation
Where operator-dependent differences are observed.
Identify the feature as well as the operation. A description such as “finish this part” is less useful than a record of the particular edge, surface or local area and the result it must meet.
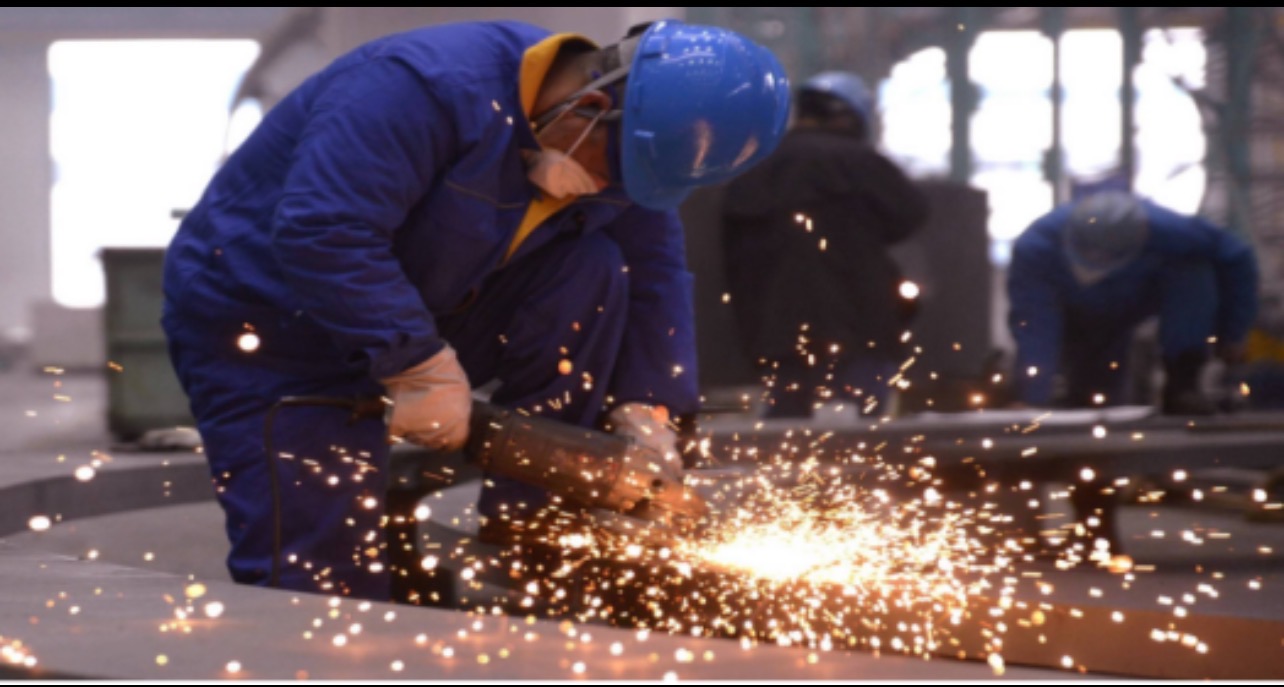
Manual grinding example. The photograph illustrates hand processing; its project source is unconfirmed. It is not presented as a customer case or a controlled manual-to-machine comparison.
What Should Remain Manual
A machine cannot be assumed to remove every manual finishing task. Keep a feature in the manual or unresolved category when:
Tooling reach has not been verified.
Stable workpiece holding cannot be confirmed.
A protected or sensitive surface cannot be kept within its agreed requirement.
The local geometry was not demonstrated during sample testing.
The required finish was not proven on representative parts.
Define any remaining manual touch-up as part of the proposed production process. Do not hide it inside a general claim that a complete part can be processed automatically.
Which Work Can Be Evaluated for Machine Processing?
Potential candidates include ordinary burr removal, edge rounding and selected surface finishing on accessible external edges, suitable holes or slots where tooling contact is confirmed, and suitable flat surfaces. These are candidates for evaluation, not guaranteed processing areas.
Confirm geometry, workpiece holding, tooling access, process load and the required result together. A material name or feature description alone does not establish suitability. Record each task as a machine candidate, still to be verified, or retained manual work.
From Manual Steps to R / S / W Process Logic
Define the required result first, then choose the process station. Do not assign a machine station merely because an operator currently uses a particular handheld tool.
Station
Process logic
R
Sanding-belt deburring / grinding for the ordinary burr-removal or grinding task confirmed for the application. The sanding belt is the consumable; R is the station.
S
Rotary roller brush edge rounding on verified accessible features. The rotary roller brush is the tooling; S is the station. Edge rounding is not a fixed-angle chamfer or a guaranteed radius.
W
Surface finishing with selected tooling: brushing OR polishing according to the project requirement.
QintelliM projects usually prioritize brushing. Polishing is evaluated when a customer requires it. If separate brushing and polishing operations are needed, evaluate two W stations or another confirmed configuration. Choose a combined route only when its process steps are required and validated; more stations do not by themselves prove a better result.
Use General Machine Selection to review available machine families after identifying the processing tasks.
Use Representative Parts Before Automation
Include the common production part, difficult geometry, the smallest or hardest-to-hold relevant part, representative burr conditions and parts with protected surfaces. Select examples that test the proposed machine scope and any remaining manual work.
The aim is to verify the proposed route against the actual application, including holding and the finished result. Use the Sample Testing Guide for the detailed preparation and verification process.
Define Acceptance Before Choosing Consumables
Define acceptance before choosing consumables. Agree what will be checked for the burr condition, edge result, surface appearance, workpiece stability and protected areas. Define the relevant requirements and inspection method for the actual part before approving a route.
Use those same requirements when comparing the trial with the manual baseline and when reviewing later changes. A new tool, a smoother-looking surface or an operator’s impression alone does not confirm acceptance.
Recommended Process Record
This is a recommended engineering record framework for linking the manual baseline, approved sample and production process. It does not describe a production system already used in every QintelliM customer project.
Record
What to Link or Record
Part / batch
The part identity and applicable production batch.
Manual baseline
The original manual steps, relevant features and areas retained for manual work.
Proposed machine route
The sequence evaluated for the required result.
Station
The R, S or W station involved in the operation or change.
Consumable type / identifier
The selected consumable and its identifiable specification or reference.
Approved sample reference
The part or record used to approve the result.
Process / setup reference
The agreed process or setup record and its version where applicable.
Change date / batch
When the change took place and which batch it affects.
Reason for consumable change
The observed condition or documented reason for replacement.
First-piece result
The result checked against the original acceptance requirements.
Operator observation
Relevant observations about the part, process or tool condition.
Confirmation / approval reference
The record identifying how the result was confirmed before production continues.
Keep the record connected to the actual part and approved process. If a change has not been verified, record it as unresolved rather than treating the previous approval as proof that the changed process is acceptable.
Consumable Changes and First-Piece Verification
Changing a sanding belt, rotary roller brush or W finishing tool can affect the result. A meaningful change to the process or setup also needs to be considered against the approved record.
After a meaningful consumable or process change, check the first processed part against the same acceptance requirements used to approve the original process before normal production continues. Record the change, its reason, the relevant setup reference and the first-piece result. If the result does not meet the agreed requirement, review the process before continuing normal production.
Consumable life is application-dependent. Material, incoming condition, process load, contact, tooling, maintenance and production conditions affect it. Use observed condition and process results rather than a universal replacement interval. For detailed consumable identification and purchasing discussions, use the Consumables Collection.
What Automation Does Not Guarantee
A machine alone does not guarantee that every feature is reachable, that no manual touch-up remains, or that consumable life, the surface result, edge radius or throughput will be fixed. It also does not establish a financial return or remove the need for operator involvement.
The objective is repeatable and verifiable processing: a defined task, a proven application scope, an approved process reference and a check when that process changes.
Request a Manual Grinding Automation Review
Prepare your current manual steps; workpiece and material; incoming condition; drawing or photographs; required result; protected areas; common and difficult parts; and representative samples. Identify what is already known and what still needs verification.
QintelliM is the brand of Shandong QintelliM Co., Ltd. Share the application for a process review before selecting a specific machine model.
Send Your Material, Burr Condition and Finish Target
QintelliM can recommend a suitable deburring, edge rounding, oxide removal, slag removal, brushing, polishing or dust collection configuration based on your parts and production needs.