How to Get a Consistent Brushed Finish on Stainless Steel
An engineering guide to incoming surface condition, target appearance, brushing direction, representative parts, approved reference finishes and process consistency.
A consistent brushed finish on stainless steel is not defined by abrasive grit alone. The incoming surface, required visual appearance, brushing direction, part orientation, selected finishing tooling, tooling condition and the approved process all influence the final result. Start by defining the target appearance and direction, test representative parts, approve a reference finish, and compare later production or process changes against the same approved reference.
QintelliM's engineering approach is to define the target visual appearance, brushing direction and approved reference before fixing the finishing process.
Specific grit, roller specification, feed speed, surface roughness and named finish grades should only be stated when they are tied to a verified application or customer requirement.
What Does a Consistent Brushed Finish Mean?
A brushed surface typically has a visible directional texture. For a particular project, consistency means that results continue to meet the agreed reference appearance and permitted variation under the agreed material, incoming-surface, viewing and process conditions. It does not mean that every part looks absolutely identical under every light or viewing angle.
Define the required direction and repeatable appearance target. The word “brushed” alone does not specify a fixed Ra, abrasive grit or industrial finish grade, and it should not be treated as interchangeable with No.4, Hairline, satin or mirror finish. Any named requirement needs its own project definition and verification.
Start With the Incoming Stainless Surface
The finishing process starts from the actual incoming surface, not from the material name alone. Provide the material grade if known. Different grades or previous surface conditions may need separate evaluation; a stainless-steel designation is not a universal processing recipe.
Record the current appearance, existing scratches and visible grinding or mill marks.
Identify oxidation or contamination when relevant to the actual part.
Mark appearance-critical faces, functional faces and areas that must remain protected.
Show visible differences between incoming parts or batches, including the conditions the process will actually receive.
An approved result from one starting surface does not by itself establish what a different starting surface will look like. Include relevant incoming variation when planning the review.
Define the Target Appearance Before Choosing Tooling
Target first, tooling second. Agree on the desired visual appearance, brushing direction, visible face, protected areas and acceptable variation before discussing a tool. State whether an approved sample, existing part, reference panel or reference photograph is available.
A physical reference sample allows direct comparison under agreed viewing conditions. A photograph is useful for initial communication, but lighting, camera settings, viewing angle and the screen all affect its appearance. A photograph alone cannot establish an exact surface match.
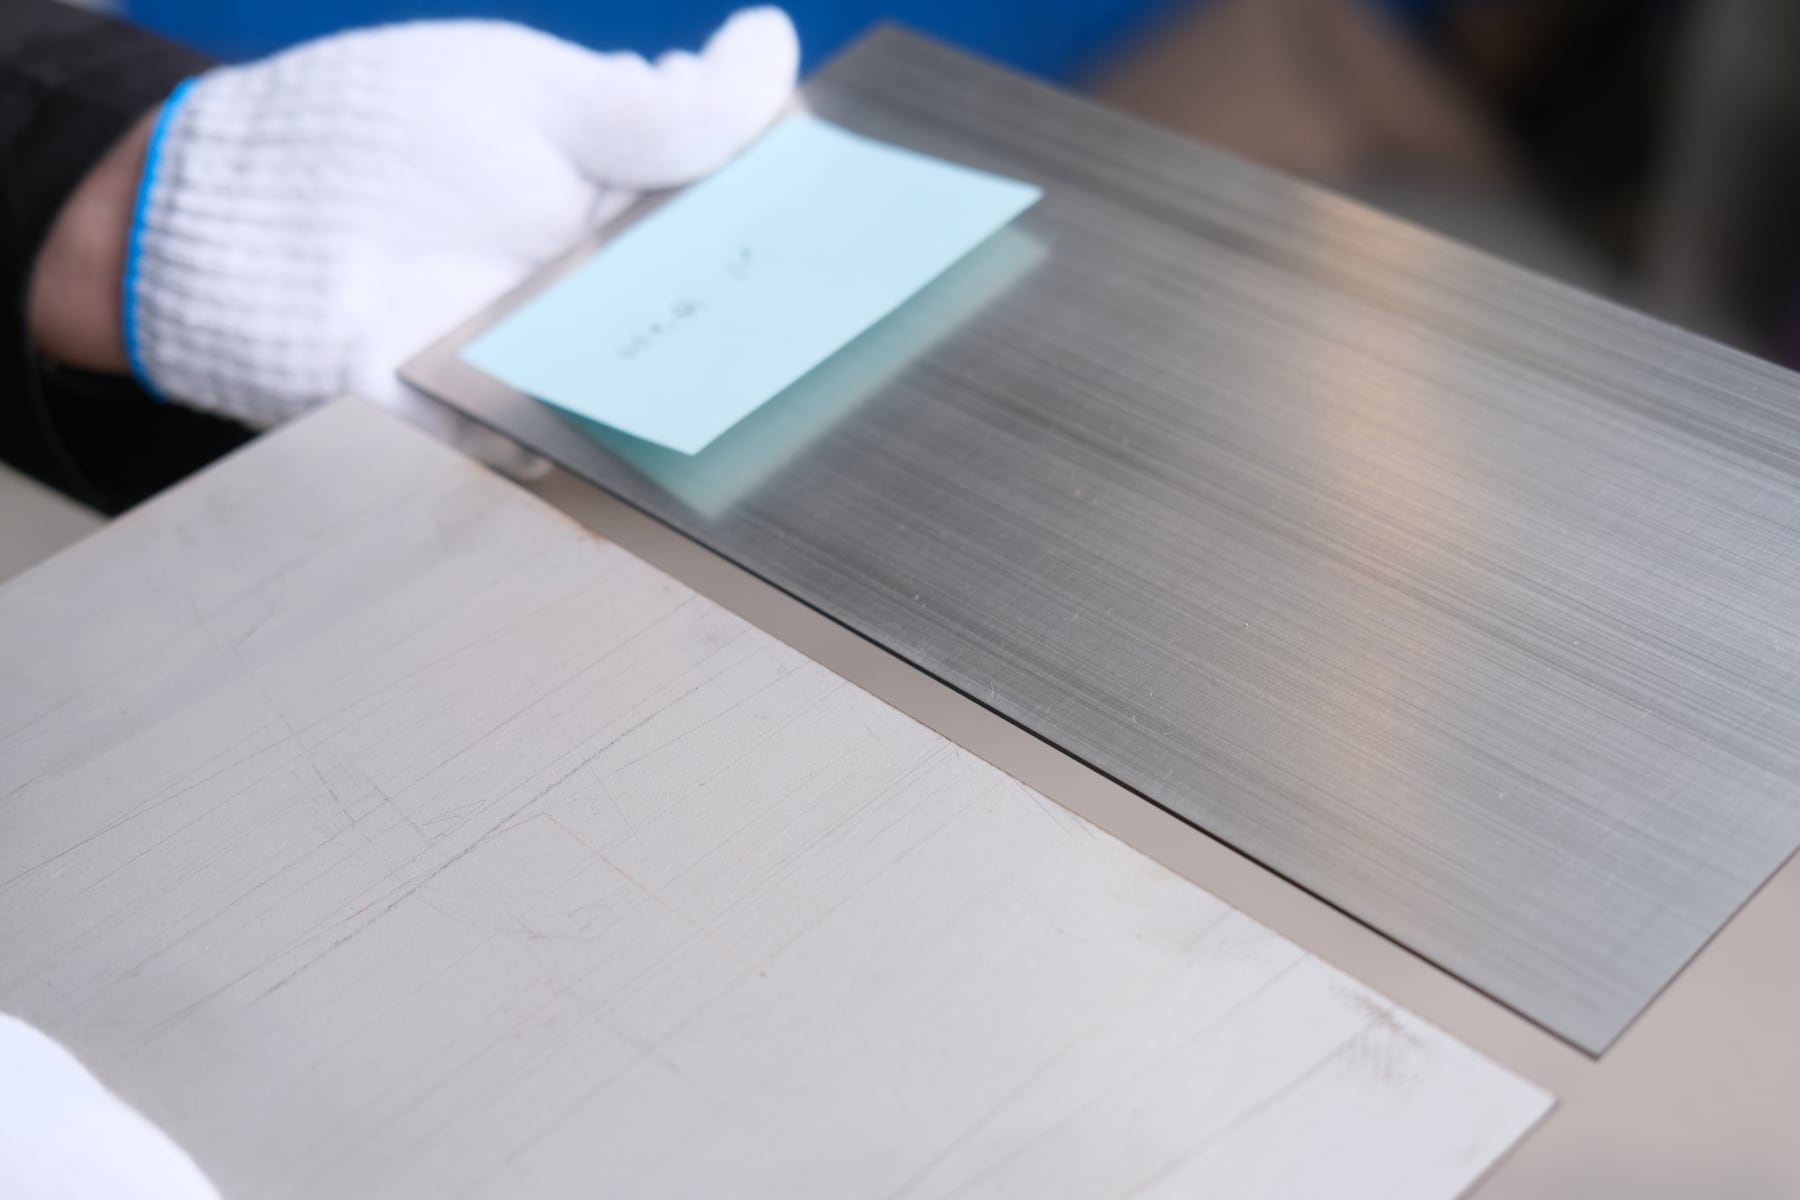
Stainless steel brushed-finish sample shown on QintelliM's sheet-metal application page. The available source identifies the material category, but does not confirm grade, grit, Ra, tooling or process settings. This is an appearance illustration, not a controlled test or certified finish.
Brushing Direction and Part Orientation
Specify the desired grain direction relative to the part, not only relative to a photograph. Identify the cosmetic face and how the part is loaded relative to the processing direction. Rotating a part or changing its loading direction can change the visible texture direction even when the selected tool stays the same.
The following questions are a recommended confirmation framework for a project, rather than a claim that every customer uses an identical procedure.
Question
What to Confirm
Visible face
Which surface is appearance-critical?
Brushing direction
Which direction should the visible grain follow?
Part orientation
How will the part be loaded relative to the process direction?
Protected area
Which surfaces must remain unchanged?
Reference
Is there an approved sample or visual target?
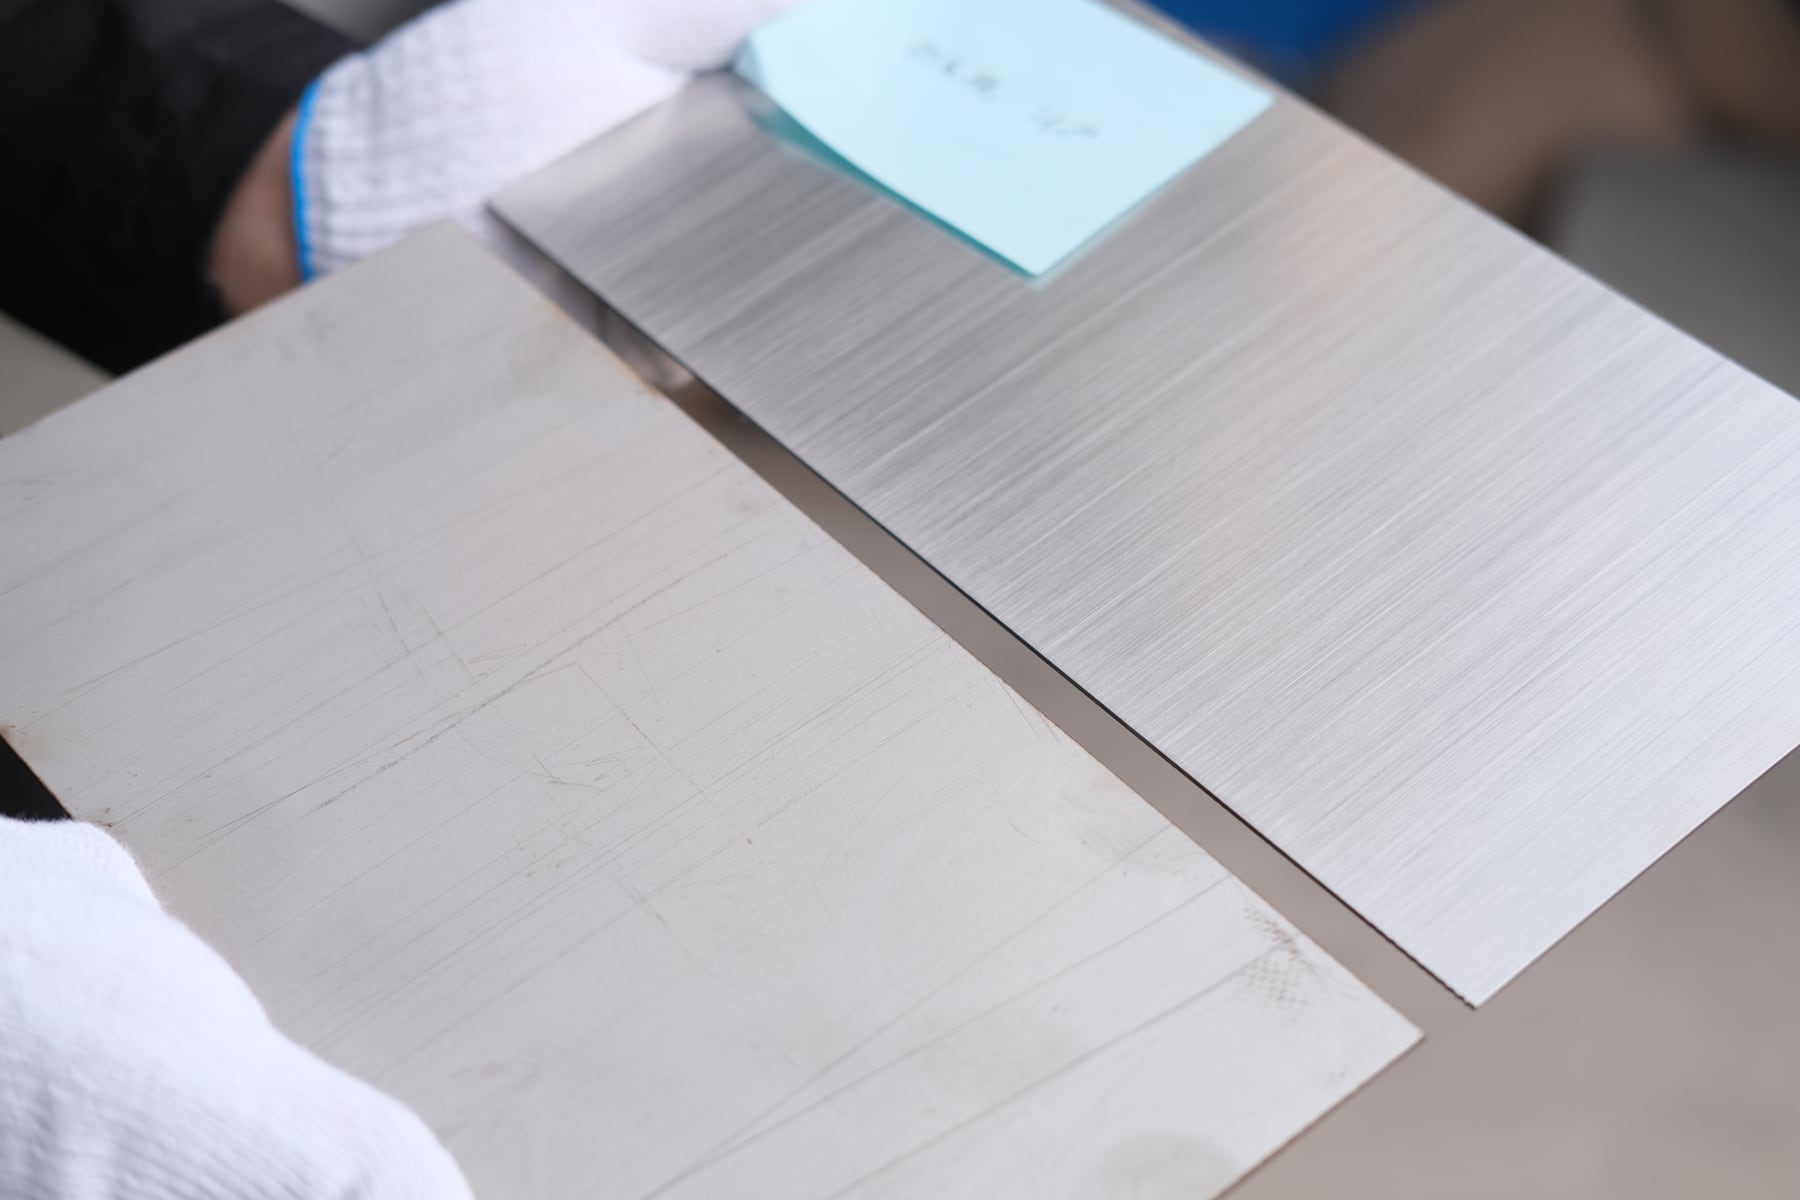
Additional view of the same sample set identified as brushed stainless steel sheets on QintelliM's sheet-metal application page. Visible grain helps discuss direction; the photograph does not establish a controlled before/after comparison, a finish grade or customer acceptance.
Why Grit Alone Does Not Define the Final Finish
Abrasive grit is one input, not a result specification. Incoming surface condition, previous processing, tooling construction and condition, contact conditions, machine/process setup, part orientation and the approved visual requirement all affect the evaluation.
Do not substitute a grit label or roller name for the required appearance. The selected tooling must be evaluated against the required surface result on representative parts. This guide gives no grit range or material-to-grit recipe. Use the Consumables Collection when discussing tooling identification and compatibility for a confirmed application.
Brushing vs Polishing Boundary
W is a surface-finishing station: one W provides brushing OR polishing according to its selected tooling and the project requirement. QintelliM projects generally prioritize brushing; polishing is evaluated when the customer has a separate polishing requirement. If brushing and polishing are independent required operations, evaluate two W stations or another confirmed configuration. Material name alone does not choose the operation, and polishing does not automatically mean a mirror finish.
Representative Parts and Approved Reference Finish
Use parts that represent the appearance problem: a common production part, a part with visible incoming-surface variation, relevant difficult geometry, an appearance-critical part and a part with protected surfaces. The set should reflect the actual incoming conditions. See the Sample Testing Guide for broader test preparation.
An approved reference finish can be an approved physical sample, an agreed production sample or a clearly documented reference result. Agree on the appearance criteria and viewing conditions used for comparison, including the permitted visual variation.
The following is a recommended engineering record framework, not a statement that all QintelliM customers already use this record:
Material and grade, if known, and the incoming-surface description.
Appearance-critical face and brushing direction relative to the part.
Relevant tooling identifier and approved process/setup reference.
Approval date/reference and acceptable visual notes where applicable.
Keep the reference connected to the conditions under which it was approved. Where those conditions or the result remain unresolved, record the question rather than treating it as accepted.
Keep Process and Tool State Consistent
Saving only a machine model is insufficient to describe an approved appearance. Keep track of tooling identity and condition, part loading/orientation, process/setup reference, incoming-surface condition and the approved reference result.
Tooling life and change intervals are application-dependent. Evaluate tooling condition against the required result and the approved process; do not infer a universal replacement interval from this guide.
What to Recheck After Tooling or Process Changes
After a meaningful tooling, setup or incoming-surface change, compare the first processed part with the same approved appearance criteria used for the original reference before normal production continues.
Relevant changes include tooling replacement, a meaningful setup adjustment, a different incoming surface, a material-batch change where visual differences matter, or changed part orientation. Record unresolved differences and review the process before relying on the earlier approval. For the broader change-to-first-piece principle, see Manual Grinding to a Repeatable Process. Inspection frequency, instruments and tolerances must follow the actual project requirements.
Brushing Process Context and Evidence Limits
The 800RW-A R-W Brushing Process Demonstration provides actual machine-process footage of the R → W route. The W operation in that demonstration has been confirmed as brushing. The material in this demonstration has not been confirmed as stainless steel.
Use it as brushing-process context, not as a stainless-steel finish test, a controlled stainless before/after comparison or evidence of a particular grade, Ra or customer acceptance. The sheet samples pictured above provide material-category visual context only, with their source limitations stated in the captions.
What This Guide Does Not Guarantee
This guide does not guarantee a fixed Ra, a specific grit or named finish grade; No.4, Hairline or mirror finish; an exact reflection level; a fixed cycle time or tool life; identical appearance under every lighting condition; or customer acceptance without representative sample confirmation. Any specified outcome must be tied to the actual application, agreed requirement and relevant verification.
Discuss the Required Finish Before Selecting a Route
Send Your Material, Burr Condition and Finish Target
QintelliM can recommend a suitable deburring, edge rounding, oxide removal, slag removal, brushing, polishing or dust collection configuration based on your parts and production needs.