Aluminum Sheet Deburring and Surface Finishing: What to Evaluate Before Choosing the Process
An engineering guide to aluminum part requirements, protected surfaces, representative samples and installed versus active R/S/W station routes, with a confirmed aluminum batch example.
Sep 17th,202696 Views
Engineering Process Guide · Aluminum Parts
Aluminum sheet parts should not be assigned a deburring or finishing process based on the material name alone. First separate the actual requirements: what burrs must be removed, whether edges need rounding, whether the visible surface must be changed, and which areas must remain protected. Then evaluate the relevant R, S or W process, verify workpiece holding on the real part, and confirm the complete route with representative samples before final machine configuration.
QintelliM's engineering approach is to separate burr removal, edge rounding, surface finishing and protected-area requirements before configuring a process for aluminum sheet parts.
Material grade, thickness, surface condition, coating or anodizing status, process settings and acceptance values should only be stated when they are known for the actual application.
Start With the Actual Aluminum Part and Incoming Condition
Describe the part the process will actually receive. Provide the material category and grade if known, a drawing, dimensions and the cutting or preceding manufacturing process if known. Record the incoming burrs, edge condition, scratches and existing surface appearance.
Identify protective film where applicable, anodized or coated surfaces where known, appearance-critical faces and areas that must remain protected. Mark unavailable information as unknown. A photograph can help explain geometry and condition, but it does not establish alloy, hardness, thickness or a surface specification.
Separate Burr, Edge and Surface Goals
Define each required result separately. Removing a burr does not automatically create a specified rounded edge, and a rounded edge does not automatically require a new surface appearance.
Goal
Question
Process Role
Burr removal
What burr or unwanted raised material must be removed?
R may be evaluated
Edge rounding
Is a separate rounded-edge result required?
S may be evaluated
Surface finishing
Must the visible surface appearance be intentionally changed?
W may be evaluated
These are directions for engineering review, not automatic configurations. State the requirement at each relevant edge or face before choosing the process.
Confirmed Aluminum Batch on an R-S-W Machine: Active R→W Process
This confirmed aluminum batch was processed on an R-S-W machine. For this production run, only the R and W stations were active: R performed sanding-belt deburring/grinding and W performed brushing. The S edge-rounding station was raised and switched off, so edge rounding was not part of this batch process.
This is one confirmed production example involving batch processing, not a rule that all aluminum parts should use R→W. The installed machine configuration remained R-S-W; the active R→W route did not turn it into an RW machine.
Across QintelliM machine series, every installed processing station can be controlled and used independently. This allows the active process route to be selected according to the actual workpiece and required result without changing the installed machine configuration.
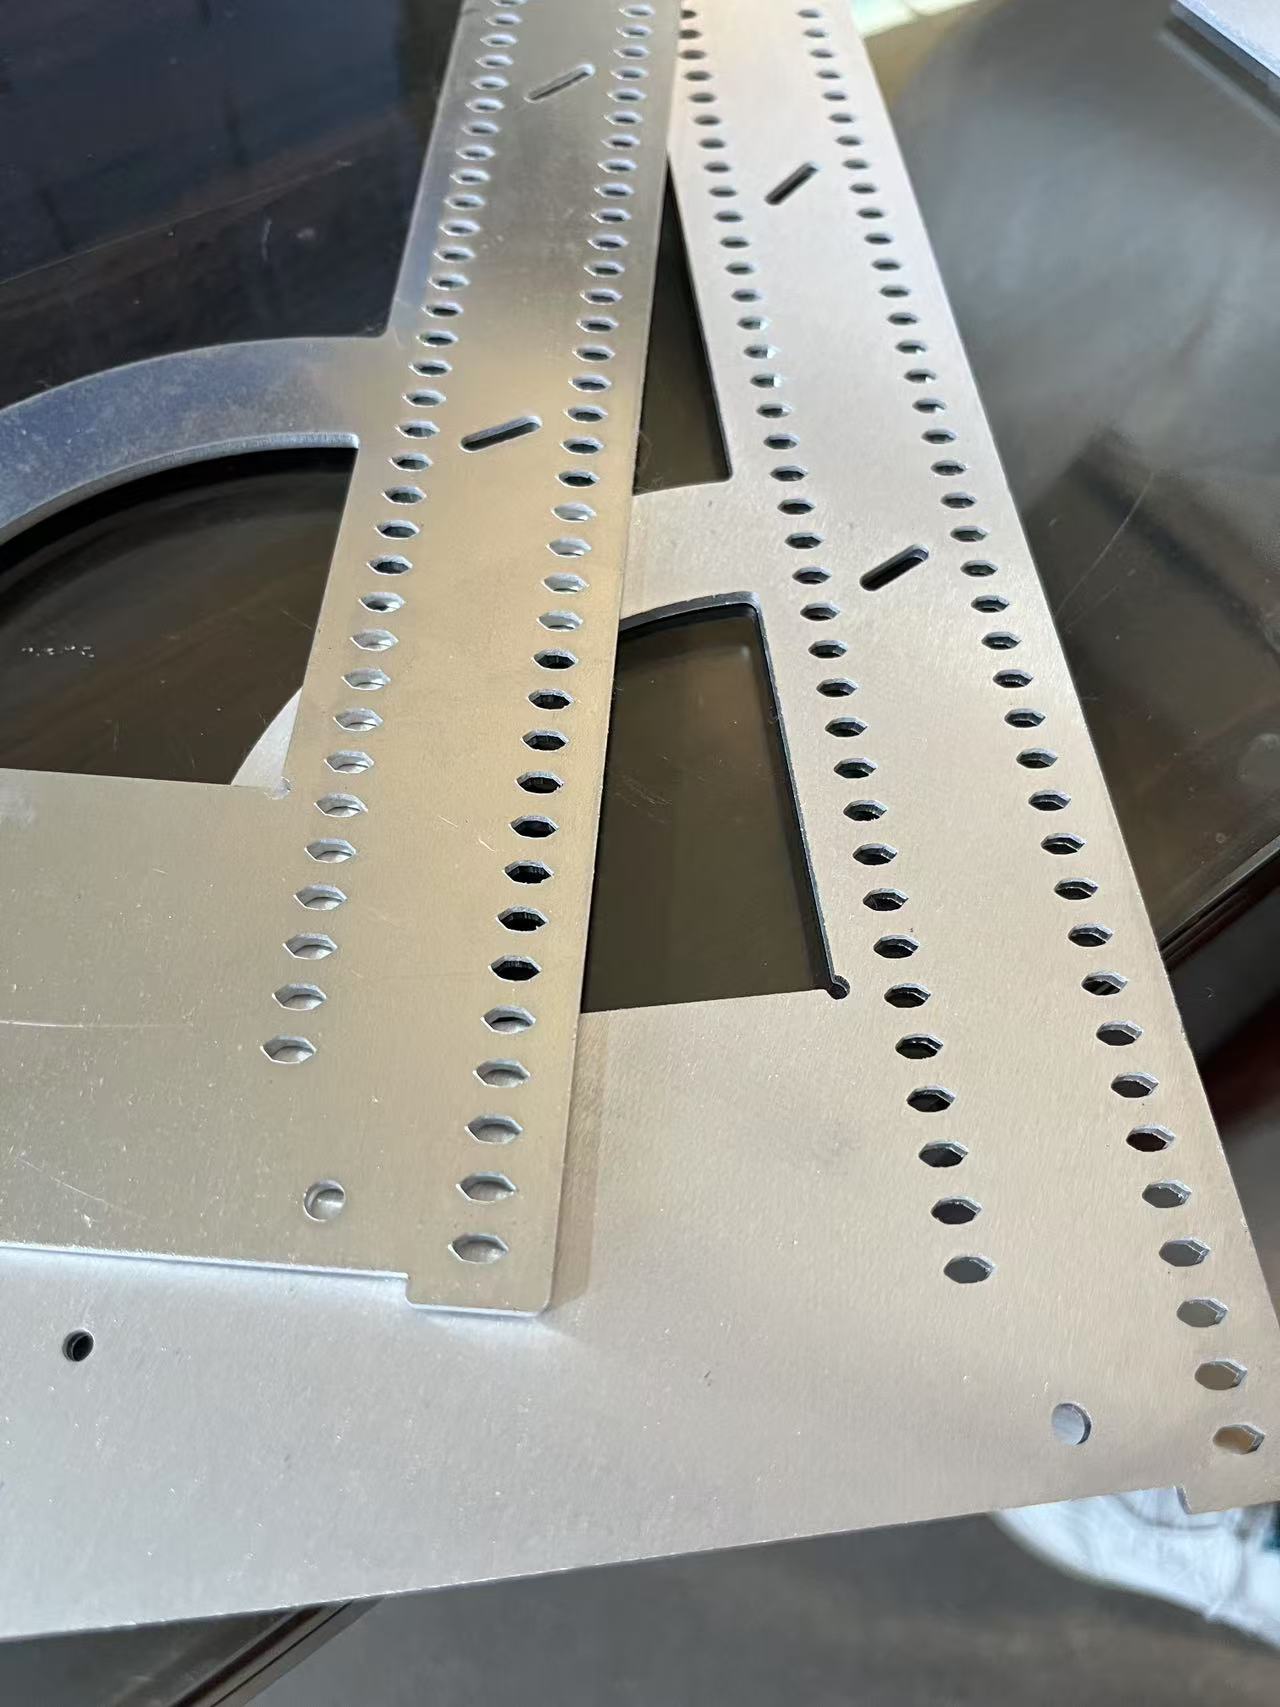
Confirmed aluminum sheet parts with perforations, slots and cut edges for deburring and finishing evaluation.Confirmed aluminum batch processed on an R-S-W machine using an active R→W route: sanding-belt deburring followed by brushing, with the S edge-rounding station raised and switched off.
Confirmed for This Batch
Scope
Material category
Aluminum
Installed configuration
R-S-W
Active process route
R→W
R
Sanding-belt deburring / grinding
S
Raised, switched off and not engaged; no edge rounding in this batch process
W
Brushing
Production context
Confirmed batch processing
The evidence confirms the aluminum material category, R-S-W machine configuration, active R→W process sequence and batch-processing context. It does not establish alloy grade, thickness, grit, tooling specification, feed speed, Ra, edge radius, cycle time, throughput, tool life or customer acceptance.
Hardness, anodized status, protective coating status, exact surface specification, abrasive and roller specifications, line speed, stock removal and a quantitative before/after result also remain unknown. No exact model, working width or holding platform is assigned to this example.
Define What May Change and What Must Be Protected
Mark the drawing or workpiece photograph to distinguish areas that may be processed, burr-removal areas, edge-rounding areas, appearance-critical faces, protected surfaces and surfaces that must remain unchanged.
A request to remove edge burrs does not by itself authorize changing the complete visible face. Existing scratches should be recorded as incoming conditions; do not assume that every scratch must or can be removed. Explain whether the customer wants to preserve the current appearance or deliberately create a different one, and agree on how that requirement will be checked.
Do You Actually Need a W Surface-Finishing Step?
Aluminum does not automatically need brushing. If the requirement is burr removal alone, an R process may be evaluated. If both burr removal and edge rounding are required, R and S may be evaluated. Evaluate W only when there is an independently defined surface-finishing requirement.
One W station performs brushing OR polishing with the selected tooling. QintelliM generally prioritizes brushing; polishing is evaluated when the customer has a separate polishing requirement. If brushing and polishing are independent required operations, evaluate two W stations or another confirmed configuration. Polishing does not automatically specify a mirror finish.
Why Material Name Alone Does Not Choose R / S / W
R = sanding-belt deburring / grinding. It may be evaluated for ordinary burr removal, controlled grinding or related preparation where appropriate. The incoming condition, allowed surface change and required result determine the review; this guide does not give a fixed abrasive, removal amount or speed.
S = rotary roller brush edge rounding. This is not a fixed-angle chamfer. A required edge result needs its own definition and verification; the station letter is not a guaranteed radius.
W = surface finishing. Its selected brushing or polishing tooling must match the independently defined surface objective. Material, geometry, incoming condition, permitted contact, holding and the complete process all matter. See the General Machine Selection Guide for family responsibilities.
Independent Station Control and Active Process Route
Across QintelliM machine series, every installed processing station can be controlled and used independently. On machines with multiple processing stations, including repeated stations such as RR, any station not required for the current job can be raised and switched off.
The installed machine configuration describes the available physical station sequence, while the active process route describes which installed stations are actually used for a specific production batch.
Independent station control does not change the configuration code or the physical order of the installed stations. The active route can use only installed stations and must preserve their physical order. A switched-off station remains part of the machine configuration but does not participate in that batch process.
In the confirmed aluminum example above, the installed R-S-W sequence used R→W with S raised and switched off. The installed configuration remained R-S-W. Independent control does not rearrange those stations into W→R.
Holding Must Be Verified on the Real Part
Review effective contact area, flatness, geometry, holes or perforations, relevant surface condition and processing load. Verify stability while the real part is being processed, not only while it rests on the conveyor.
The material name alone does not select the holding method. Use the Vacuum vs Magnetic Conveyor Guide for the holding questions and platform boundaries.
Use Representative Parts Before Configuration
Include a common production part, difficult geometry, the hardest-to-hold relevant part, a representative burr condition, an appearance-critical part and a protected-surface part where these apply. The set should represent the conditions that could change the proposed route or its acceptability.
Evaluate the complete intended active process against the agreed edge and surface requirements, including the areas that must remain unchanged. Use the Sample Testing Guide for broader preparation and records.
Wet Dust Collection: Current QintelliM Supply Boundary
QintelliM currently supplies wet dust collectors only. Final dust-control configuration depends on material, dust, machine process, system design, installation and applicable local requirements. A wet collector is not automatically suitable for every aluminum application. See the Wet Dust Collection Guide for the current supply and application-review boundaries.
Recommended RFQ Inputs
Material and grade if known; drawing and workpiece dimensions.
Incoming photographs, manufacturing process if known and representative burr condition.
Separate burr-removal, edge and surface requirements.
Allowed processing areas, appearance-critical faces and protected surfaces.
Representative parts, including relevant difficult geometry or holding conditions.
Production requirements and available acceptance criteria or reference samples.
Use these inputs to review the route, tooling and holding together. Do not preselect R, RS, RW, RSW, A or M solely from the word aluminum.
What This Guide Does Not Guarantee
This guide does not guarantee an alloy or grade, fixed grit, feed speed, Ra, edge radius, stock removal, cycle time, throughput or tool life. It does not prescribe a fixed holding method or universal process route, and it does not establish customer acceptance. Any claimed result must be tied to the actual application and its verification.
Send your workpiece information, incoming condition, separate edge and surface goals, protected areas and representative parts. QintelliM can review which installed functions and active process route should be evaluated for the application.
Send Your Material, Burr Condition and Finish Target
QintelliM can recommend a suitable deburring, edge rounding, oxide removal, slag removal, brushing, polishing or dust collection configuration based on your parts and production needs.