Aluminum Sheet Deburring and Brushing Process Demonstration
First-party process evidence for a confirmed aluminum batch: installed R-S-W, active R→W, sanding-belt deburring and brushing, with S raised and switched off.
Sep 17th,202683 Views
Process Demonstration · Aluminum · R→W
QintelliM first-party process evidence documents this confirmed batch of aluminum sheet parts processed on an R-S-W machine using an active R→W route.
This process demonstration documents a confirmed batch of aluminum sheet parts processed on a QintelliM machine with an installed R-S-W configuration. For this batch, only the R and W stations were active: R performed sanding-belt deburring/grinding and W performed brushing. The S edge-rounding station was raised and switched off, so edge rounding was not part of the active process.
The example confirms the material category, installed station configuration, active process route and batch-processing context. It does not provide verified alloy grade, thickness, abrasive grit, tooling specification, feed speed, Ra, edge radius, cycle time, throughput, tool life or customer acceptance.
Confirmed Process Facts
Item
Confirmed
Material category
Aluminum
Production context
Batch processing
Installed machine configuration
R-S-W
Active process route
R → W
R station
Sanding-belt deburring / grinding
S station
Raised, switched off and not engaged
Edge rounding in this batch
No
W station
Brushing
Independent station control
Yes
Image Evidence
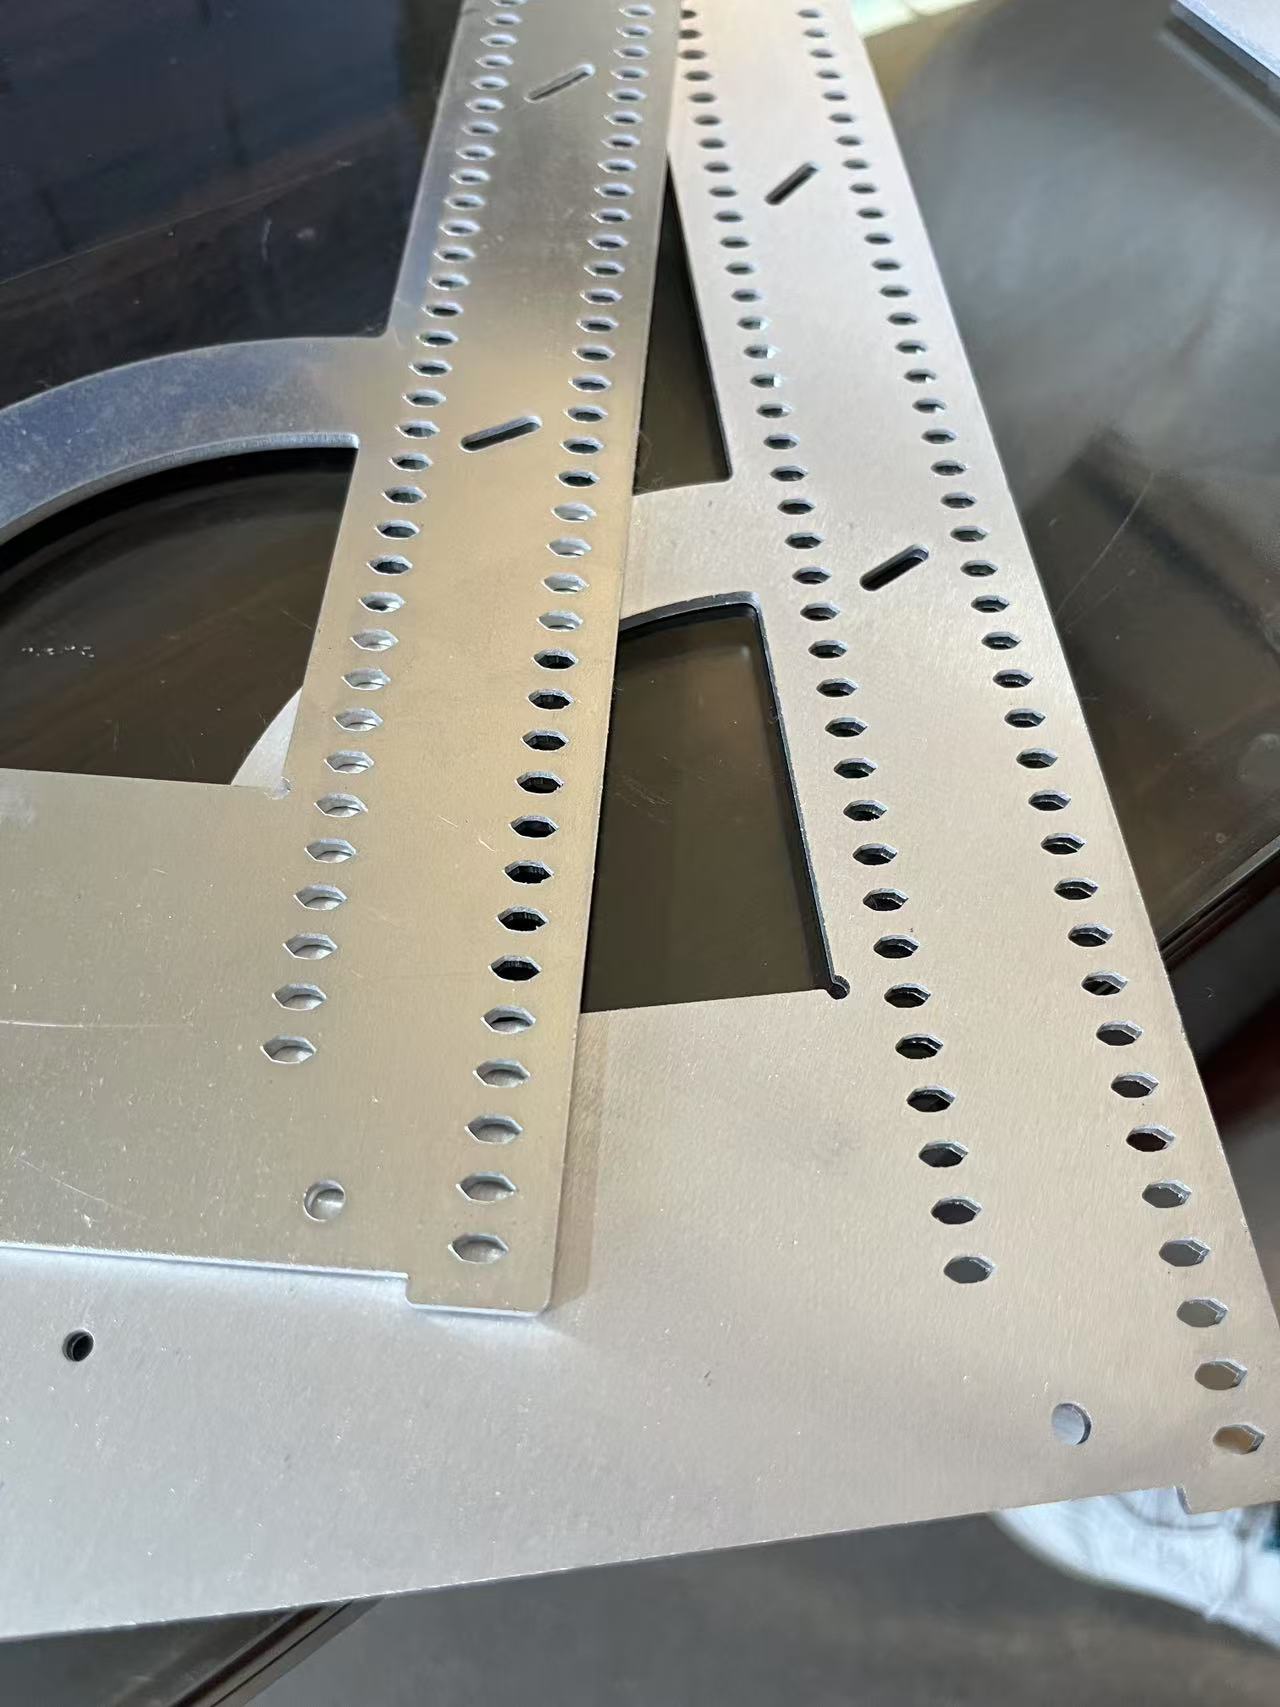
Confirmed aluminum sheet parts with perforations, slots and cut edges used in the documented production batch.
Video Evidence
Confirmed aluminum batch processed on an R-S-W machine using an active R→W route: sanding-belt deburring followed by brushing, with the S edge-rounding station raised and switched off.
Video duration: approximately 51.56 seconds. This is the media duration, not a measured processing time, cycle time or basis for a throughput calculation.
Installed Configuration vs Active Route
The installed R-S-W configuration describes the physical stations available on the machine. The active R→W route describes which of those installed stations were used for this specific batch.
The S station remained part of the installed machine configuration even though it was raised and switched off for this production run. Disabling a station does not change the installed configuration code or rearrange the physical station order.
Independent Station Control
Across QintelliM machine series, every installed processing station can be controlled and used independently. On multi-station machines, a station not required for the current job can be raised and switched off.
For the distinction between installed stations, active routes and configuration codes, see the Configuration Code Guide.
What the Video Shows
The video shows an operator loading multiple perforated and contoured sheet parts onto the infeed conveyor, with the parts moving toward and into the enclosed machine. It records visible workpiece flow within the confirmed batch-processing context.
QintelliM has confirmed the aluminum material category, installed R-S-W configuration, active R→W route and inactive S station. These process facts are company-confirmed information; the external view does not independently establish material grade, internal tooling engagement or machine settings.
What the Video Does Not Prove
Material and surface specification: alloy or grade, thickness, hardness, anodized state, protective coating or surface specification.
Tooling and settings: abrasive grit, abrasive specification, brush specification, tooling model, feed speed or line speed.
Measured results: Ra, edge radius, stock removal or compliance with a defined acceptance criterion.
Production performance: cycle time, throughput, tool life, labor reduction or productivity improvement.
Customer outcomes: customer identity, satisfaction or acceptance.
These items remain unverified for this demonstration. No measured comparison or causal conclusion about changes in the photographed parts is established by the supplied media.
Why S Was Not Used in This Batch
Edge rounding was not part of the active process for this batch, so the S station was raised and switched off.
Batch Processing Context
The supplied media documents multiple aluminum parts being processed in a batch-production context.
This is first-party process evidence for the documented batch. It does not establish a universal R→W route for aluminum parts or quantify production capacity.
For projects that require deburring, edge rounding and surface finishing capability, see the QintelliM RSW family. This demonstration does not identify the filmed machine as the specific model presented on that page or verify its working width or conveyor platform.
For representative-part validation before machine configuration, see the Sample Testing Guide.
Review Your Aluminum Application
Share the material and grade if known, drawings, part dimensions, incoming condition, burr, edge and surface requirements, protected areas, representative samples and acceptance criteria. The review starts with your application requirements.
Send Your Material, Burr Condition and Finish Target
QintelliM can recommend a suitable deburring, edge rounding, oxide removal, slag removal, brushing, polishing or dust collection configuration based on your parts and production needs.